
Key Sourcing Takeaways
- Closed-loop two-part platinum LSR injection (85T & 120T presses) forms burr-free rims and angled air-release pinholes without secondary punching.
- Ventilated secondary post-curing (typically 200 °C × 4 h) drives volatile weight loss ≤ 0.5%, followed by washing and packing in our 150–200 m² clean zone.
- Operated under ISO 13485:2016 (62026Q00072R100) batch traceability; finished-device FDA/EU registrations belong to the commercial brand owner.
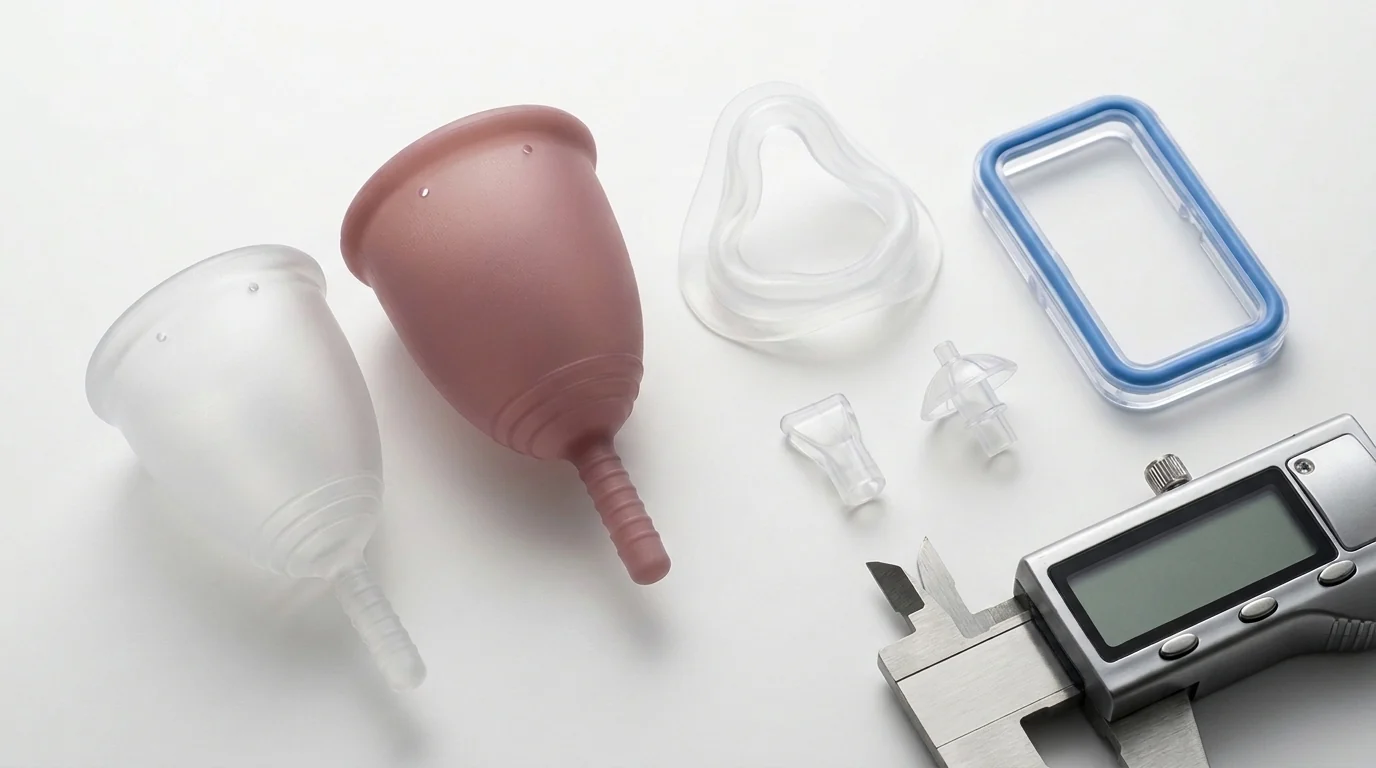
Modern silicone menstrual cups are manufactured via closed-loop Liquid Silicone Rubber (LSR) injection molding using sourced medical-grade, two-component platinum-cured elastomer rather than open-mill solid rubber compression. Precision stainless-steel LSR molds form the bell wall, smooth upper sealing rim, internal milliliter graduations, grip stem, and angled air-release pinholes in one virtually flash-free shot, followed by ventilated oven secondary post-curing (typically 200 °C × 4 hours) and washing, 100% illuminated inspection, and sealed packaging inside a dedicated clean zone under ISO 13485 batch traceability.
Menstrual cups are one of Dongguan Youbang's core custom product specialties (~50,000 pcs/month typical cup production capacity; ~110,000 pcs/year historical shipment volume across European and North American brand programs, tracked separately from capacity). Below is how engineering, tooling, curing, and compliance come together from CAD to mass production.
1. LSR Injection Molding vs. HCR Compression Molding for Menstrual Cups
Why do feminine-care brands specify Liquid Silicone Injection Molding on 85T and 120T presses over legacy solid-silicone (HCR) compression molding?
| Manufacturing Parameter | Liquid Silicone Rubber (LSR) Injection Molding | Solid Silicone (HCR) Compression Molding | Direct Impact on Intimate Comfort & Hygiene |
|---|---|---|---|
| Elastomer Feed System | Sealed 1:1 barrel pumping of two-part platinum-cured LSR | Open-roller milling and hand-loaded gum charges | Closed-loop LSR feed minimizes airborne dust or fiber inclusions |
| Upper Rim Parting Line | Virtually flash-free precision steel shut-off | Visible overflow flash requiring manual knife/scissor trimming | Avoids microscopic hand-trimmed ridges against sensitive vaginal mucosa |
| Suction-Release Pinholes | Molded directly in-tool (typically 1.2–2.0 mm angled core pins) |
Often punched manually after molding with hollow needles | Molded-in smooth holes resist tearing and prevent rough crevices that trap biofilm |
| Wall & Pop-Open Consistency | High tear strength, low compression set, ±0.05 mm precision shut-offs |
Greater wall-thickness variation across split mold halves | Consistent bell unfolding ("pop-open") and leak-free seal across boiling cycles |
| Multi-Firmness SKU Flexibility | One precision steel mold can often run both Soft (~35A) and Classic (~45A) LSR |
Separate milled rubber batches with higher setup scrap | Lets brands launch Sensitive and Active firmness SKUs from one mold investment |
2. Step 1: Selecting Biocompatible Platinum LSR & Shore A Durometer
Because a menstrual cup contacts internal mucosa for up to 8–12 hours per wear cycle, raw-material purity and durometer tuning drive both safety and customer retention:
- Sourced Medical-Grade Platinum LSR: Youbang sources two-component addition-cured liquid silicones from tier-one suppliers (Wacker, Shin-Etsu, Momentive, Dow, Elkem, Dongjue, Zheng'an) formulated without BPA, ortho-phthalates, natural rubber latex proteins, or organic peroxides, supported by upstream polymer ISO 10993-5 (cytotoxicity), ISO 10993-10 (irritation/sensitization), and USP Class VI raw-material data.
- Compliant Liquid Color Masterbatches: Whether molding translucent clear cups or custom pastel shades, liquid silicone pigments are selected for heavy-metal-free REACH and biocompatibility compliance.
- Tuning Shore A Firmness (
40 ± 5 Shore ATypical Window):- Soft / Sensitive (
30–38 Shore A): Folds effortlessly and reduces bladder pressure, paired with a slightly reinforced upper rim radius so the bell still opens reliably. - Classic / Active (
40–50 Shore A): Delivers crisp pop-open recovery against stronger pelvic floor muscles. Because linear shrinkage varies minimally between adjacent LSR grades, we verify both durometers duringT1sampling (typically 7–15 days).
- Soft / Sensitive (
3. Step 2: Engineering the Precision Menstrual Cup Steel Mold
At Youbang, DFM and mold structure design are engineered in-house while hardened stainless-steel CNC machining and cavity texturing are completed with specialized Dongguan toolmakers (customer-funded molds remain 100% owned by the customer, with NDA protection available):
- Parting-Line Placement & Lapped Shut-Offs: Positioning the parting line along a controlled upper-rim transition and lapping shut-off lands prevents liquid silicone bleed.
- Angled Molded-In Vent Pins: Retracting or precision-fitted core pins form 2 to 6 smooth suction-release holes beneath the rim without secondary punching.
- Micro-Matte Exterior vs. Smooth Interior: A controlled matte EDM texture on the outer bell and grip stem eliminates tacky skin drag during insertion, while a smooth inner wall rinses clean effortlessly.
- CNC-Engraved Volume Lines & Size Marks: Internal milliliter lines and brand/size reliefs are machined directly into the steel core—never printed with surface ink.
- Pre-Tooling 3D Prototype Check: Once requirements are clear, the quotation is confirmed, and 2D/3D CAD is complete, we provide 1–3 free 3D-printed engineering samples (shipping paid by buyer) to confirm bell ergonomics and stem geometry before cutting steel.
4. Step 3: Closed-Loop LSR Molding, 200 °C × 4 h Post-Curing & Clean Packing
Mass production (typically 15–30 days after sample sign-off) follows a documented four-stage workflow:
- 1:1 Closed-Barrel Metering & Vulcanization: Sealed A and B LSR drums pump through a cooled static mixer with metered liquid pigment directly into heated cavities on our 85T or 120T LSR presses, curing rapidly into high-elongation thermoset cups before careful manual gloved demolding.
- Ventilated Secondary Oven Post-Curing: Every molded lot is baked in ventilated convection ovens—typically around
200 °Cfor4 hours, adjusted by grade and wall thickness—driving off residual cyclic siloxanes so volatile weight loss stays ≤ 0.5% with zero chemical odor. - 150–200 m² Clean Washing, Inspection & Packaging Zone: (Transparency note: molding occurs in our dedicated LSR press shop, not a classified cleanroom molding room.) Post-cured cups enter our 150–200 m² clean assembly and packaging area (equipped with air shower and gowning buffer) for purified washing, drying, 100% illuminated rim and vent-hole inspection, and sealed pouching.
- Dimensional & Durometer QC: Shift samples are verified on our 2D optical coordinate measuring system (
×1) and Shore A durometers (×3) underIQC → IPQC → FQC → OQCcontrols.
5. Step 4: ISO 13485 Traceability vs. Brand Regulatory Registrations
Clear regulatory responsibility protects both manufacturer and brand owner:
- Youbang's Factory Scope: Certified ISO 13485:2016 (
62026Q00072R100, silicone product manufacturing excluding licensing-required products; valid through2029-03-24), linking raw-material lot → production batch → post-cure log → outbound shipment ID, plus coordination of finished-part SGS, Intertek, or TÜV chemical/biocompatibility testing (typically ~10 days). - Brand Owner's Commercial Registration: Product-level market clearances—such as US FDA 21 CFR 884.5400 establishment registration / 510(k) or EU national filings—belong to the commercial brand owner; Youbang holds no FDA/CE product registrations and provides the manufacturing traceability dossier to support your regulatory submissions.
Technical & Regulatory References
- U.S. FDA eCFR — 21 CFR § 884.5400 Menstrual Cup Classification
- Elkem Silicones — Liquid Silicone Rubber (LSR) Processing & Healthcare Overview
Explore our Quality & Certifications scans or compare Free Engineering Samples to start your custom menstrual cup review.