Manufacturing Capabilities · Dongguan

Custom Silicone Molding,
from Compounding to Verified Parts

Dongguan Youbang operates 2 LSR injection molding machines (85T & 120T), 10 solid HCR compression presses (200–250T, 400×400 to 650×650 mm platens), and primer-bonded overmolding for customer-supplied inserts—backed by documented post-curing and batch traceability.

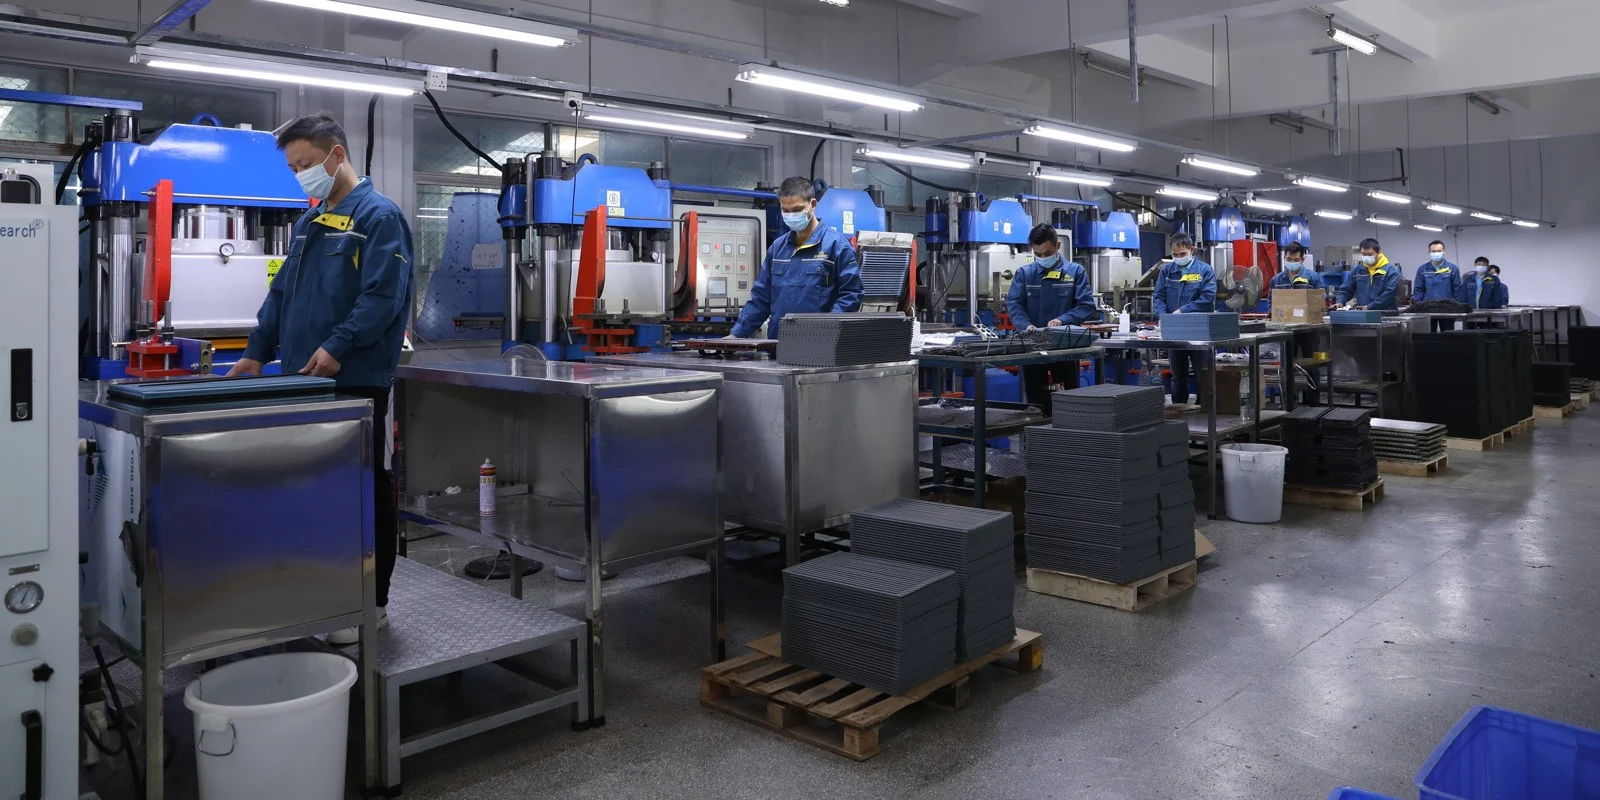
Youbang molding workshop
01
Since 20114,000 m² Dongguan plant
02
85T & 120T LSR2 liquid injection machines
03
10 × 200–250T HCR400×400–650×650 mm presses

Core Silicone Molding Routes

Select the Molding Route Around Geometry, Volume & Inserts

85T & 120T Presses × 2Min Wall 0.25 mm (0.30 mm Stable)Precision Fit ±0.05 mm Typical

LSR injection molding (85T & 120T)

Two-component platinum-cured liquid silicone is closed-loop metered, mixed, and injected into precision steel cavities. Capable of thin walls down to 0.25 mm (0.30 mm stable mass production) and precision feature tolerances typically ±0.05 mm (evaluated per part).

Explore LSR injection molding (85T & 120T) specs →

CAD Inputs & Selection Criteria

Recommended Inputs: 3D STEP + 2D tolerance drawing, target Shore A hardness, gate-mark exclusion zones, and annual forecast.

Does your geometry have micro-vents, thin membranes (0.25–0.30 mm), or flash-sensitive sealing rims that justify precision LSR tooling?
200–250T Presses × 10Platens 400×400 to 650×650 mmMin Wall 0.40 mm (0.50 mm Stable)

HCR compression molding (200–250T, 400×400–650×650 mm)

Pre-milled solid silicone charges are weighed and compression-cured across 10 hydraulic presses. Supports wall sections down to 0.40 mm (0.50 mm stable mass production), custom Pantone batches, and large-footprint mats or multi-cavity consumer parts.

Explore HCR compression molding (200–250T, 400×400–650×650 mm) specs →

CAD Inputs & Selection Criteria

Recommended Inputs: Part envelope, wall thickness, cosmetic parting-line boundaries, Shore A target, and order quantities by color.

Where can a hand-trimmed parting line sit without affecting sealing, appearance, or tactile comfort, and how many cavities match your batch size?

Customer PC / PP / PA / SS / Al / CuSilane Primer Chemical BondingMechanical Interlock & Shutoff Control

Primer-bonded insert overmolding (PC, PP, PA & metals)

Silicone is molded onto customer-supplied PC, PP, PA, stainless steel, aluminum, or copper inserts using surface treatment and primer bonding inside LSR injection or HCR compression tooling.

Explore Primer-bonded insert overmolding (PC, PP, PA & metals) specs →

CAD Inputs & Selection Criteria

Recommended Inputs: Insert 3D/2D CAD, exact resin grade or alloy, heat deflection limit, primer keep-clear zones, and trial insert allowance.

Can your supplied insert withstand molding clamp pressure and curing heat without warping, and how will peel or pull retention be verified on T1 samples?

Interactive Engineering Tool

LSR Injection vs. HCR Compression Route & Tooling Estimator

Select four project parameters to compare the recommended molding route, relative tooling investment multiplier, typical T1 lead time, and prefill your RFQ brief.

Engineering Reference · Confirmed per CAD
1. Estimated Annual Volume
2. Application & Compliance
3. Geometry & Construction
4. Current Documentation Stage
Recommended Molding Route

Multi-Cavity Platinum HCR Compression Molding

Ideal for 3,000–30,000 pcs consumer brand runs: keeps tooling investment ~50–70% lower than cold-runner LSR while utilizing 400×400 to 650×650 mm presses and custom Pantone compounding.

Relative Tooling Multiplier
2.0× – 3.5× (vs. 1.0× 1-cavity pilot tool)
Elastomer & Post-Process
Food-contact platinum-cured HCR + ~200 °C × 4 h ventilated post-curing
Typical Sampling & Production
Free 1–3 pc 3D geometry check (if eligible) · New mold T1 7–15d · Mass 15–30d
Request Quote with This Spec Final cavity count, tolerances and pricing are confirmed against your drawing.

Shop-Floor Workflow from Compounding & Molding to Post-Cure & QC

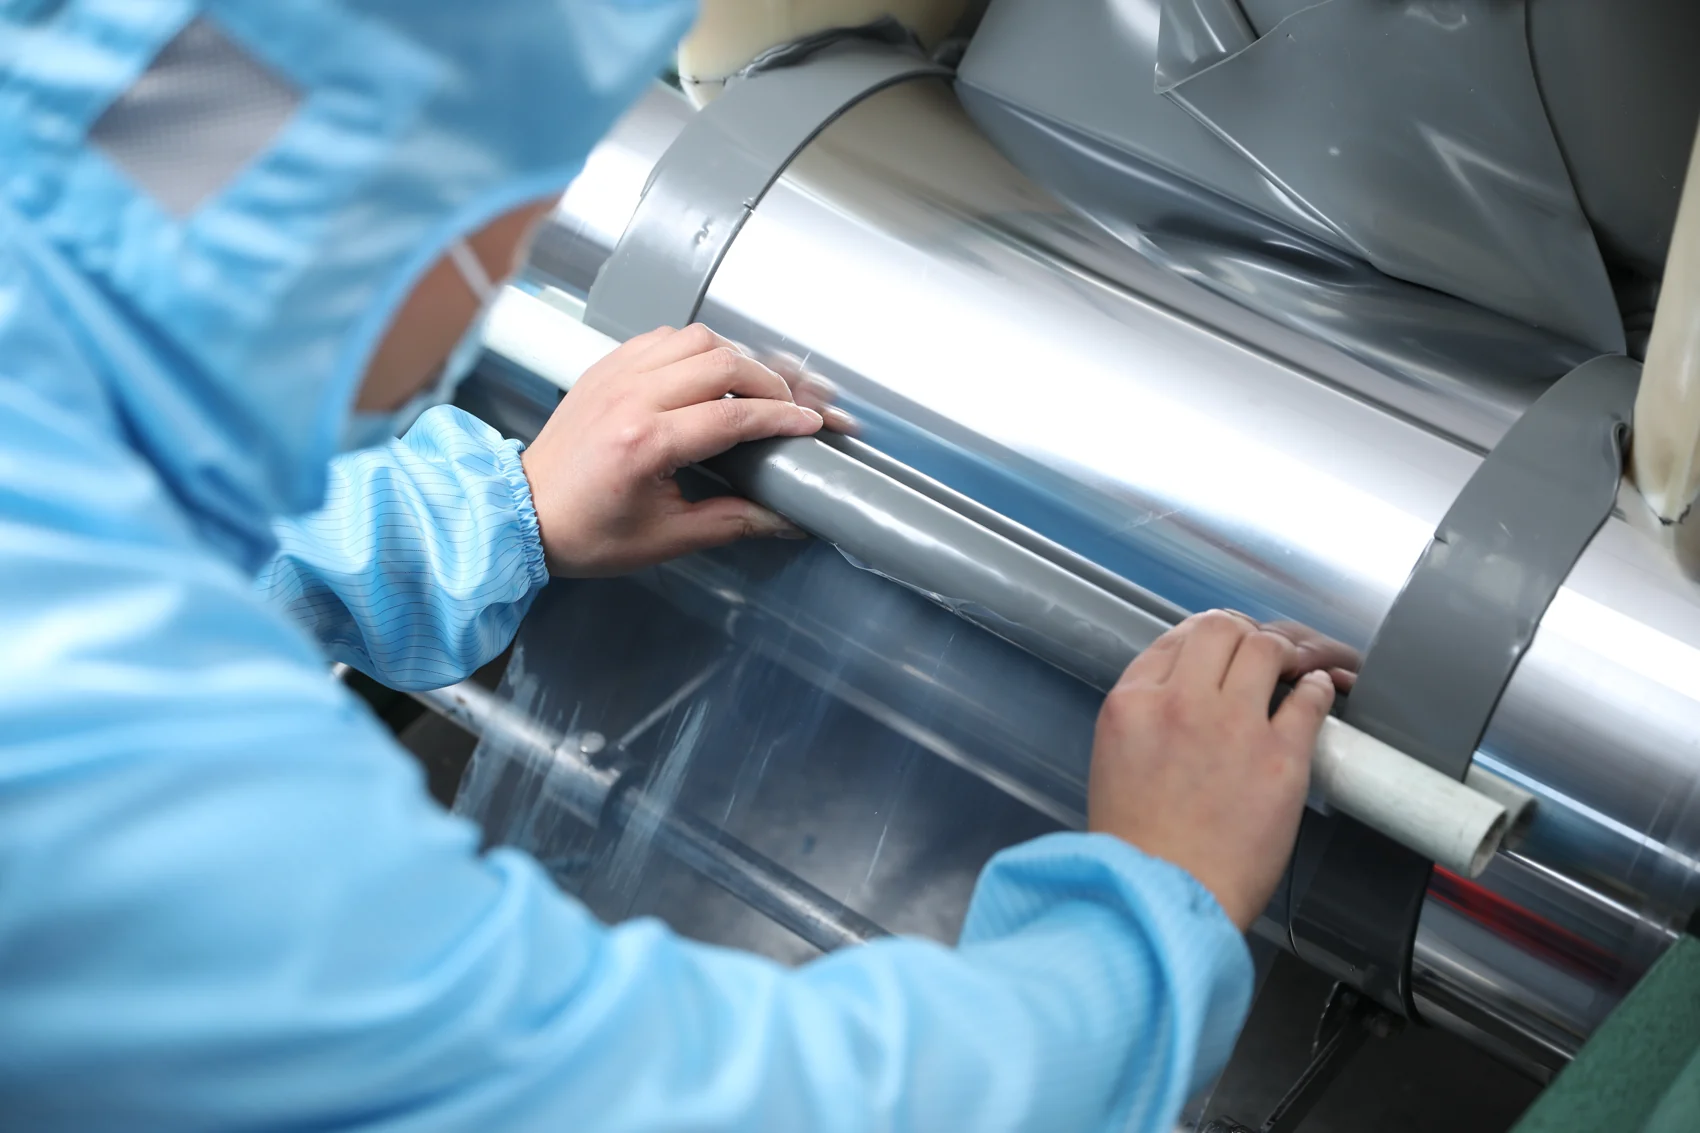
Compound milling & Pantone matching
Rubber compound processing on rollers
01

Compound milling & Pantone matching

Blending elastomers from Wacker, Shin-Etsu, Momentive, Dow, Elkem, Dongjue, and Zheng'an on 2 open mixing mills with in-house Pantone matching (reported ΔE ≤ 1.5; confirm conditions per project).

Molding and handling process — factory footage
02

Mold loading & vulcanization

Weighing preforms, loading heated cavities, and demolding cured parts manually with operator flash inspection (footage shows HCR compression molding).

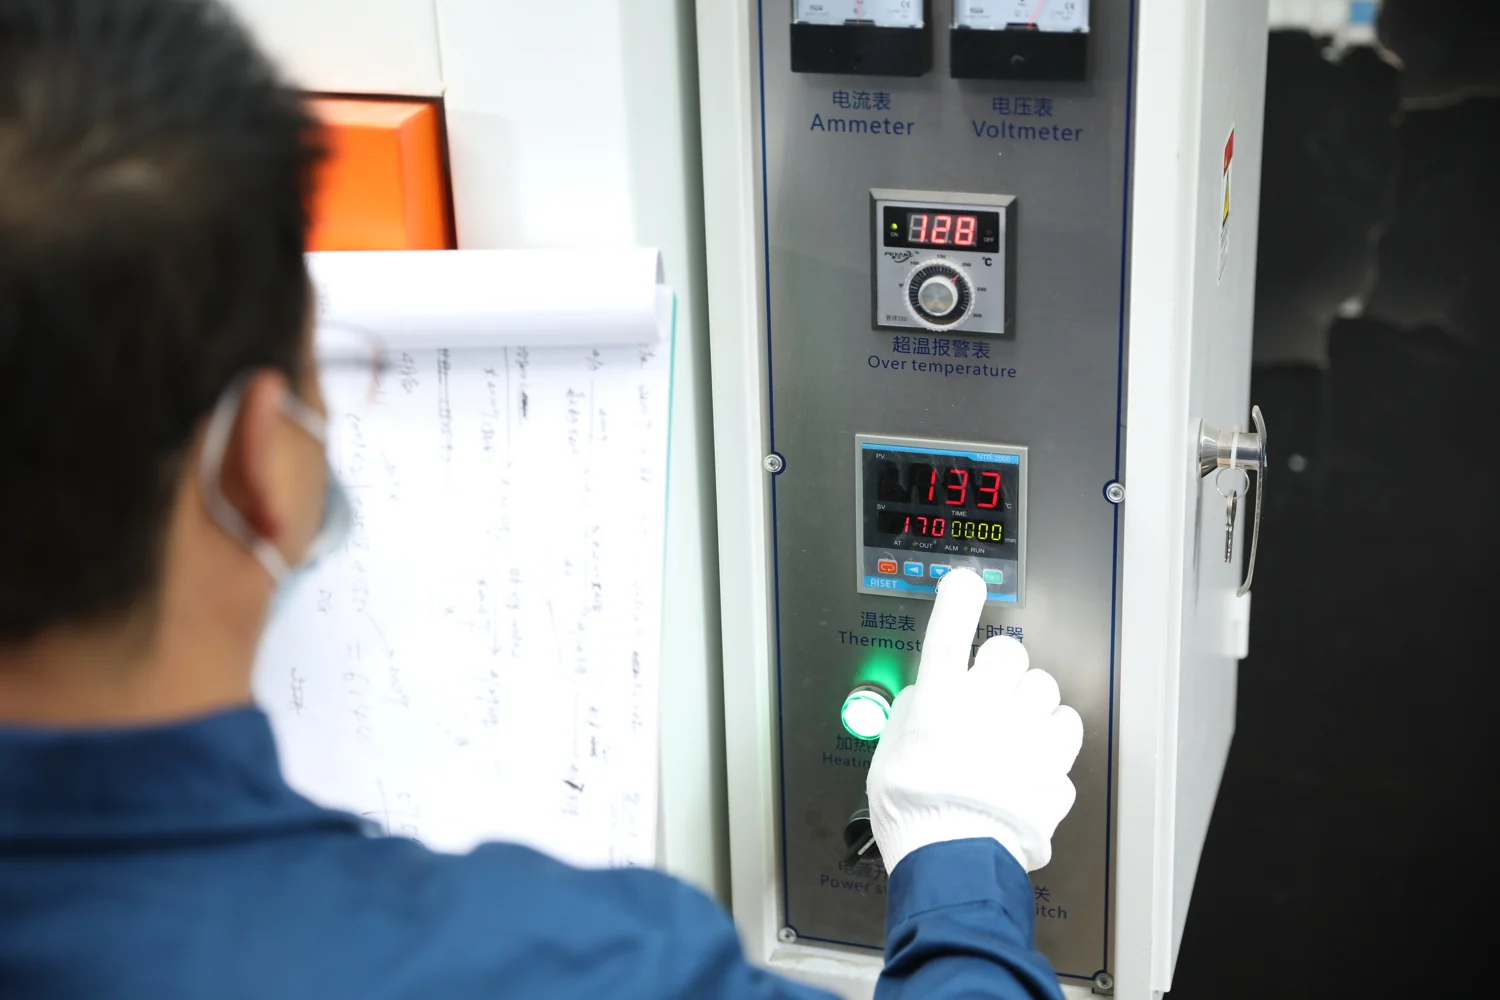
Ventilated oven secondary post-curing
Oven operation
03

Ventilated oven secondary post-curing

Secondary baking—typically 200 °C for ~4 hours in ventilated ovens, adjusted by grade and wall thickness—to stabilize properties and meet ≤ 0.5% LFGB volatile loss requirements.

Optical & Shore A inspection
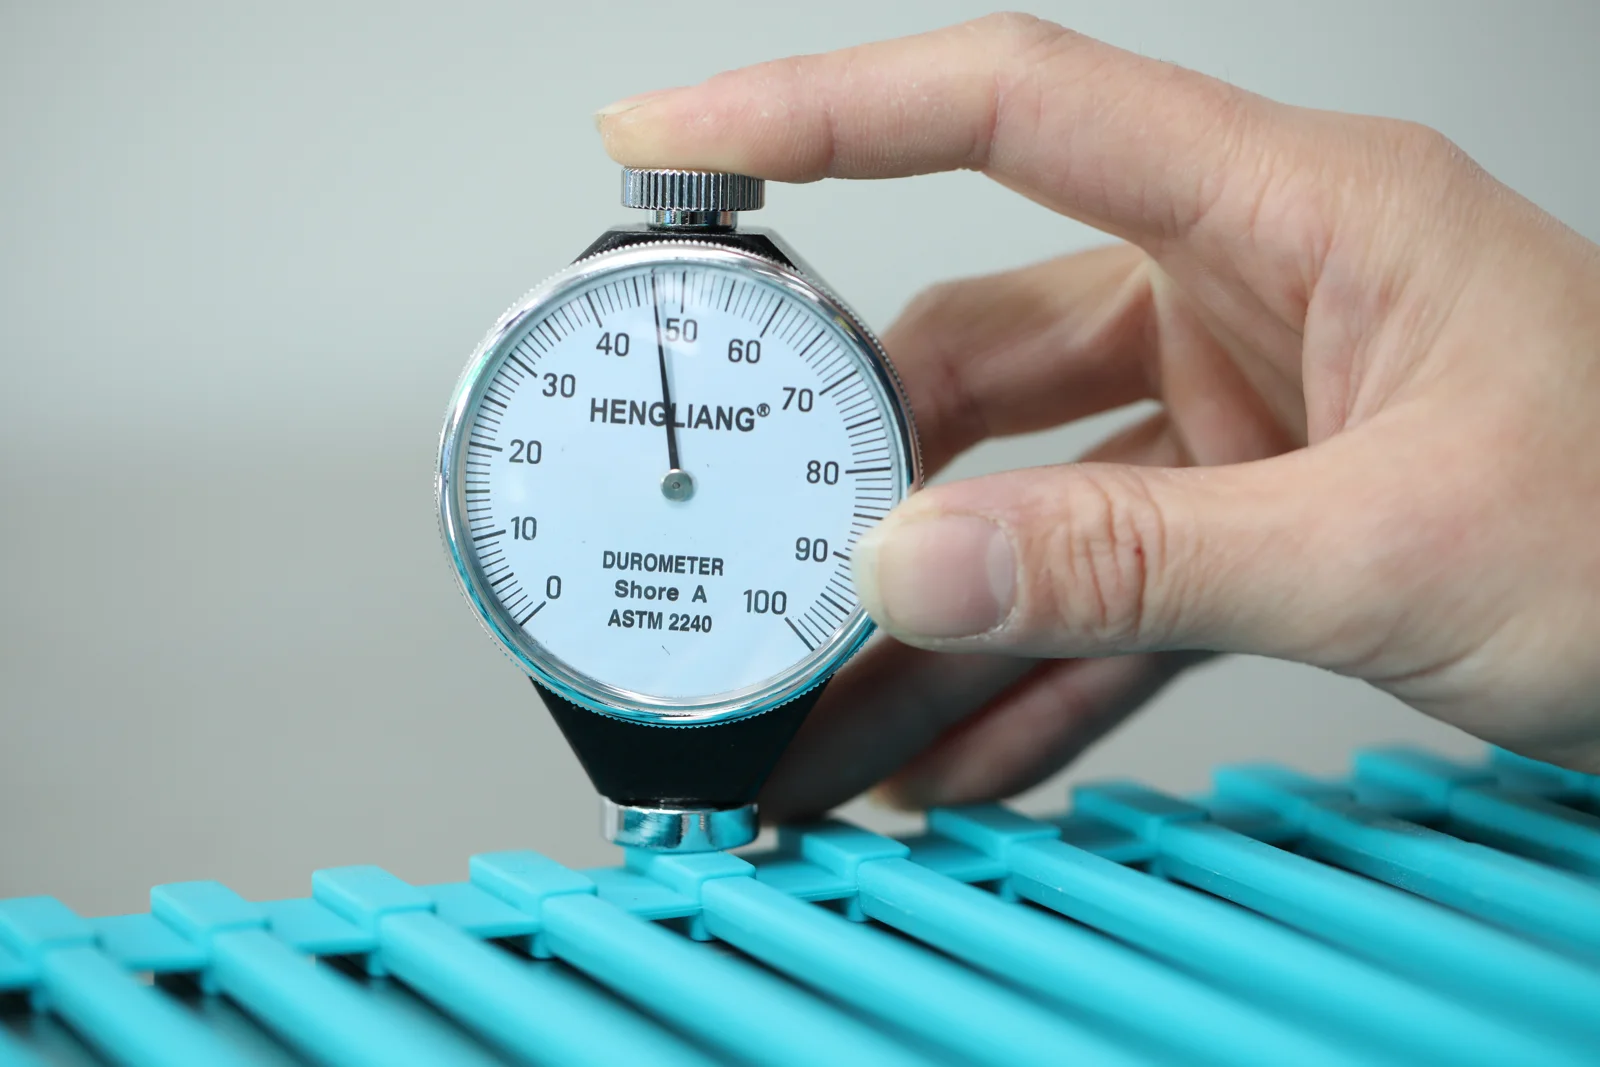
Local hardness check on a roll-up rack
04

Optical & Shore A inspection

Dimensional checks on our 2D optical measuring system and hardness verification across 3 Shore A durometers under IQC, IPQC, FQC, and OQC controls.

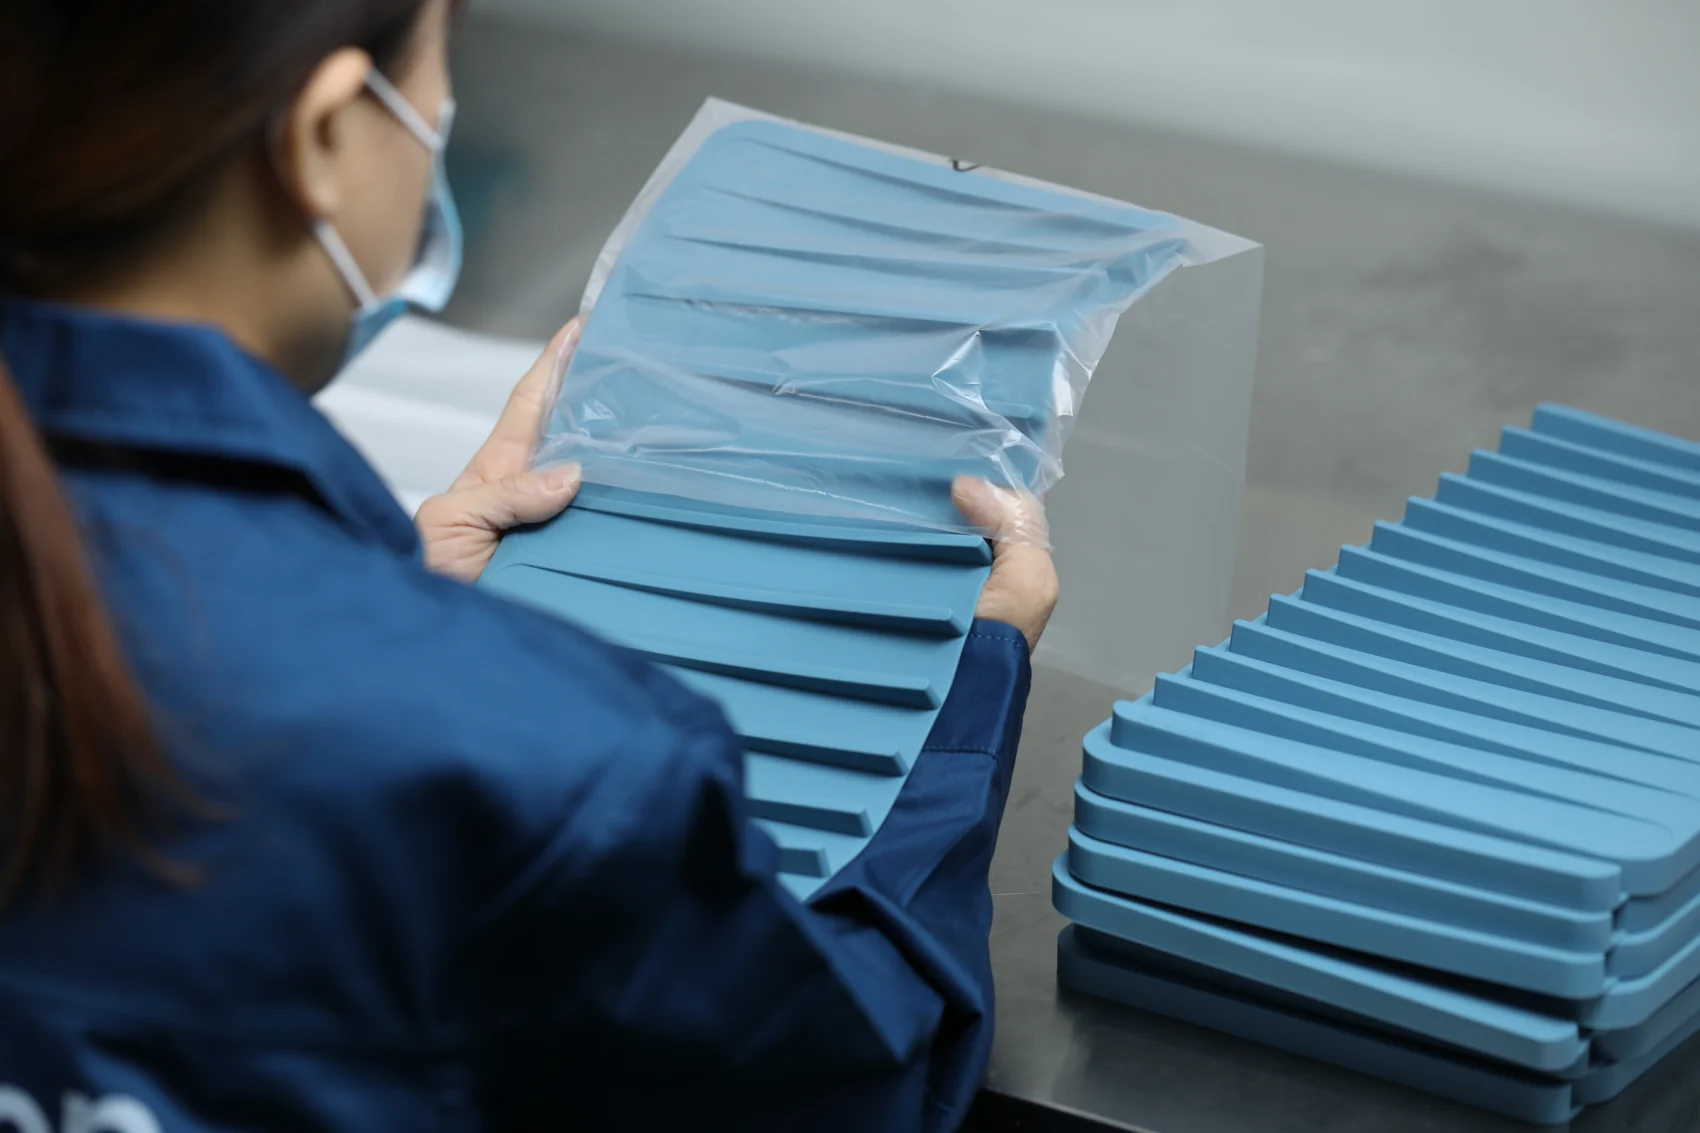
Clean washing, assembly & packing
Packing molded dish-drying mats
05

Clean washing, assembly & packing

Packing standard consumer goods on dedicated lines, plus a 150–200 m² clean washing, inspection, assembly, and packaging area for medical and personal-care silicone parts.

Clear boundary between in-house operations and partner processes

Handled In-House at Youbang

  • LSR injection (85T, 120T), HCR compression (10 × 200–250T) & primer overmolding
  • Compound milling (2 open mills), Pantone color matching & ventilated post-curing
  • In-house DFM & mold design, screen printing, soft-touch coating & 150–200 m² clean assembly/packing

Coordinated with Specialist Partners

  • CNC mold steel machining & EDM/matte/gloss cavity texturing
  • Laser etching and epoxy doming secondary decoration
  • Custom retail boxes, blister trays, pouches & third-party SGS/Intertek/TÜV lab testing (~10 days)

Evaluated capability per part (not a blanket guarantee across all geometries): 0–80 Shore A hardness (commonly 30–70A); ±0.05 mm typical precision feature tolerance (±0.1–0.2 mm standard molded features); 0.25 mm min / 0.30 mm stable LSR wall; 0.40 mm min / 0.50 mm stable HCR wall; PC, PP, PA, stainless steel, aluminum, and copper primer-bonded overmolding. New mold T1 samples typically 7–15 days; mass production typically 15–30 days.

Connect process parameters to lot-level traceability

Operated under ISO 9001:2015 (21424Q0270R1S) and ISO 13485:2016 (62026Q00072R100), linking raw-material lot numbers, production batches, post-cure records, and outbound shipment IDs.

  • ISO 13485 & ISO 9001
  • Lot-to-shipment link
  • 2D optical & Shore A QC
Quality documents & scope →

B2B Factory Direct · 24h Engineering & Tooling Review

Match your part drawing to the right molding route

Send 2D/3D CAD files, target Shore A hardness, compliance standard, and order quantities by color for a 24-hour engineering review.

✓ NDA available before CAD exchange✓ Eligible for 1–3 free 3D fit prototypes✓ Paid molds 100% owned by customer

Direct Dongguan Engineering Desk

  • Accepts STEP / IGES / PDF / DWG or sample photos
  • New mold T1 typically 7–15 days · Mass run 15–30 days
  • Direct Tel / WeChat: +86 185 6655 6911 (Zhou Li)