
Enclosure & Fluidic Seals
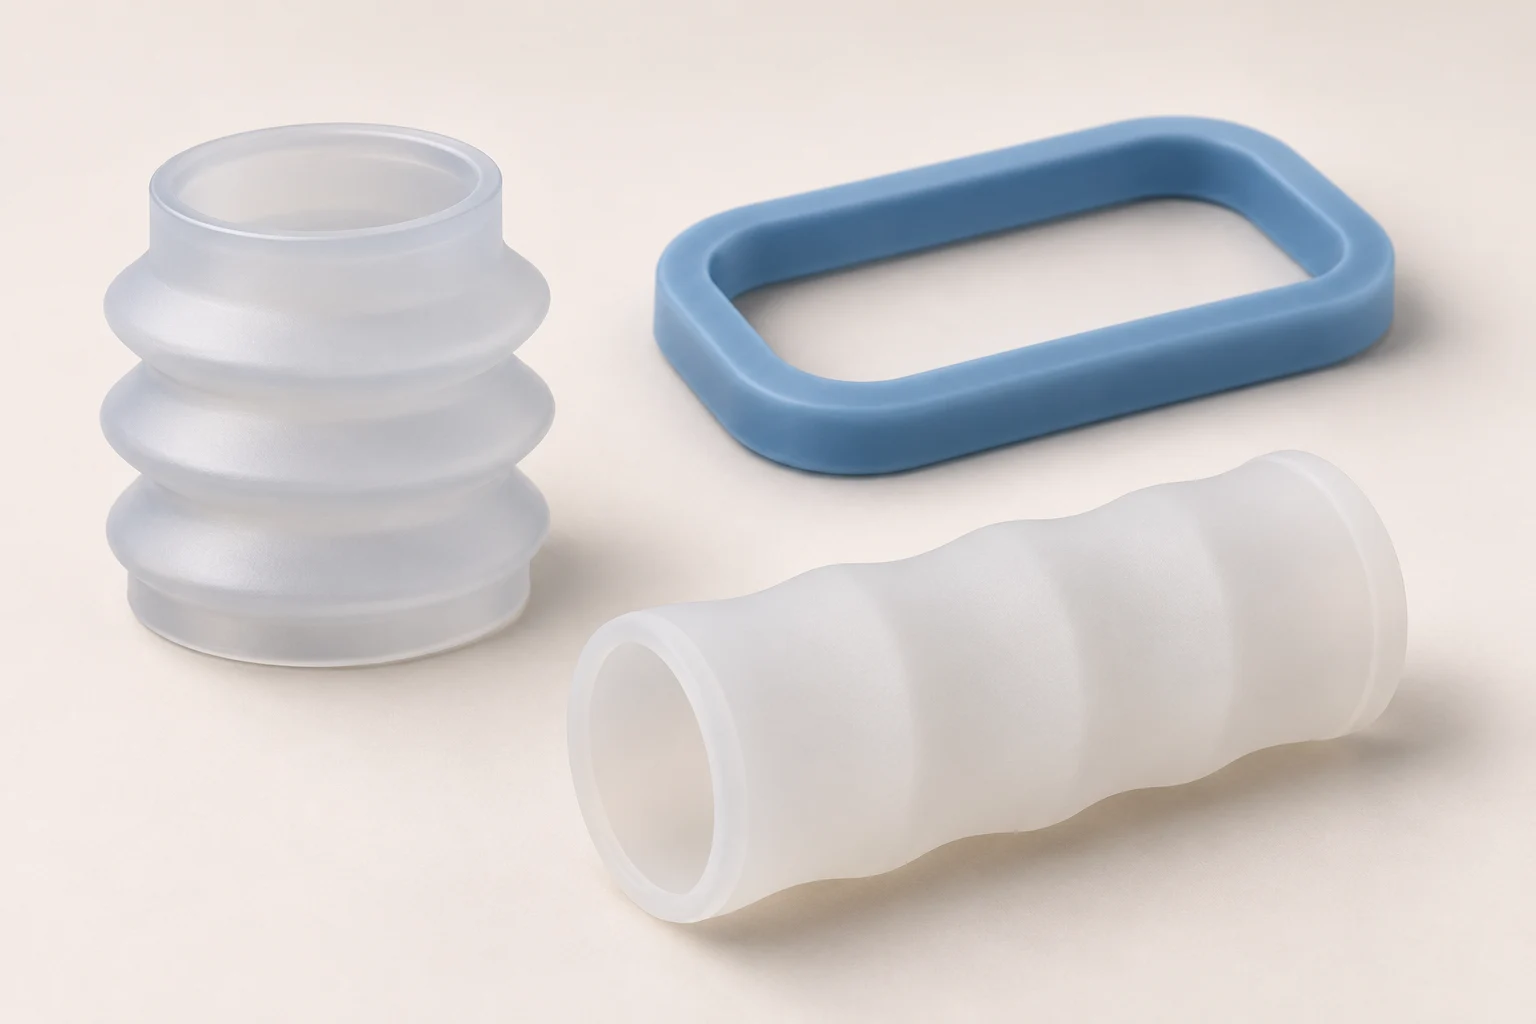
Perimeter gaskets, diagnostic cartridge stoppers, and primer-overmolded frames (30–70 Shore A common; ±0.05 mm typical precision tolerance) seal mating housings against fluid ingress and wipe-down disinfectants.
Youbang · B2B Custom Silicone Manufacturing · Dongguan
Dongguan Youbang Silicone Products Co., Ltd. manufactures custom non-implantable silicone seals, respiratory cushions, fluidic valves, and primer-overmolded interfaces to your 2D/3D device drawings. Operating under ISO 13485:2016 (62026Q00072R100) with 85T/120T LSR presses, ten 200–250T HCR presses, 200 °C × 4 h post-curing, and a 150–200 m² clean assembly area, we align elastomer processing and batch traceability with your engineering and quality teams.
ISO 13485:2016 Certificate 62026Q00072R100 (valid 2026-03-25 → 2029-03-24) covers Dongguan Youbang Silicone Products Co., Ltd. for the production of silicone products, excluding products requiring qualification licensing. Youbang delivers raw-lot → molding-batch → shipment traceability, post-curing logs, upstream elastomer CoA/SDS/USP Class VI/ISO 10993 summaries (Wacker, Shin-Etsu, Momentive, Dow, Elkem), and ~10-day SGS/Intertek/TÜV test coordination; the device OEM holds finished-device FDA 510(k)/establishment registration and EU MDR CE authorization.
View certificate scans and scope →Perimeter gaskets, diagnostic cartridge stoppers, and primer-overmolded frames (30–70 Shore A common; ±0.05 mm typical precision tolerance) seal mating housings against fluid ingress and wipe-down disinfectants.
Duckbill, umbrella, and cross-slit valves plus diaphragm boots molded on 85T/120T LSR machines regulate airflow and reagents, with slit geometry and rebound validated on T1 molded samples.
CPAP/nasal mask skirts (LSR thin walls down to 0.25 mm min / 0.30 mm stable), stethoscope ear tips, and hearing-aid domes combine low-durometer comfort with 200 °C × 4 h ventilated post-curing (≤ 0.5% volatiles).
Part CAD is only the starting baseline—align contact duration, disinfection chemistry, supplied substrates, and verification splits before cutting prototype steel.
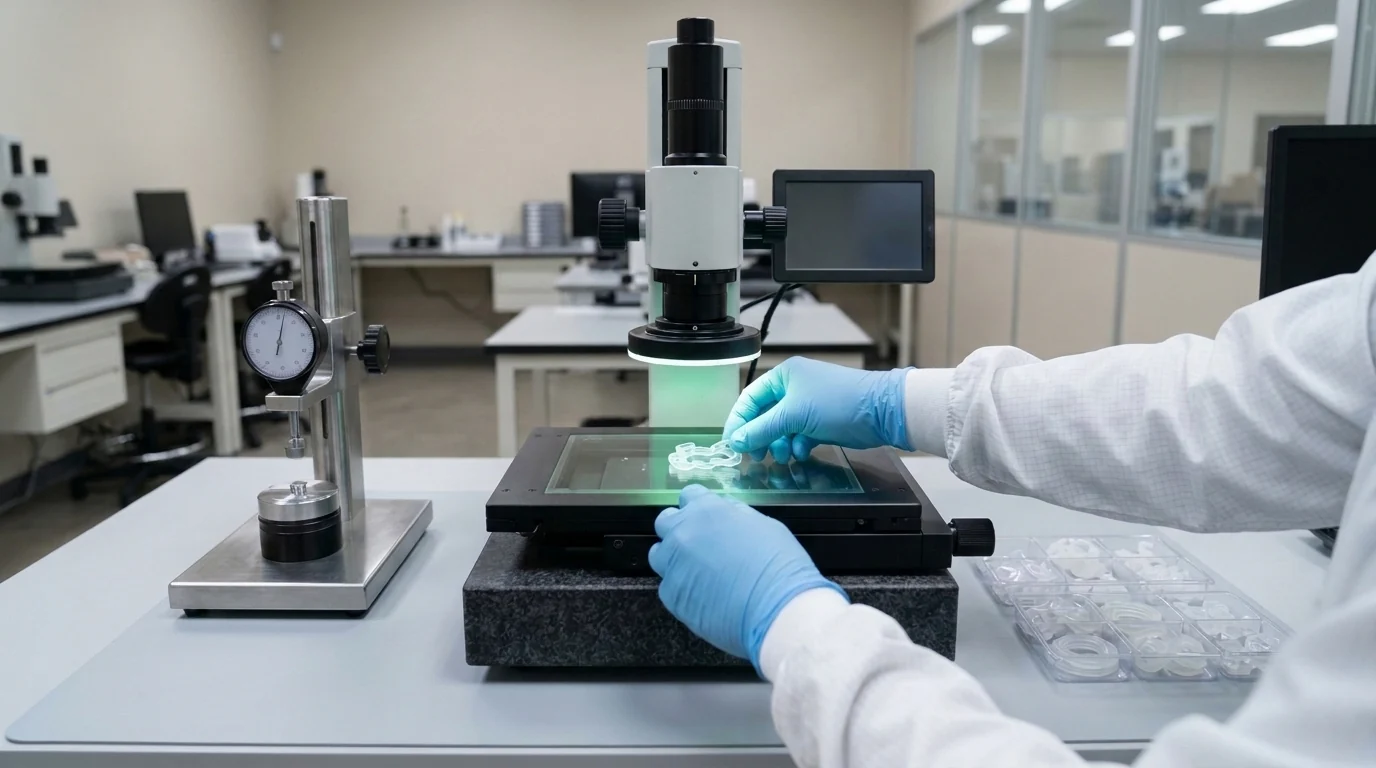
Supplier qualification requires clear visibility into how parts are measured, washed, and packed—without overstating facility classifications.
Sourcing & Tooling FAQ
Covering CAD readiness, custom MOQ evaluation, free 3D fit checks vs. T1 silicone samples, NDA protection and mold ownership.
Send your drawing or sample photo directly to Zhou Li’s engineering desk for a 24h DFM reply.
No. ISO 13485:2016 Certificate 62026Q00072R100 certifies Dongguan Youbang Silicone Products Co., Ltd.'s quality management system for silicone product production (excluding products requiring qualification licensing). Complete-device FDA 510(k), establishment registration, and EU MDR CE marking belong to the device owner, supported by our batch traceability, FAI, and upstream elastomer dossiers.
Yes. Provide the brand, exact grade, upstream datasheet, and projected EVT/production volume so our purchasing and molding teams can confirm lead time, minimum elastomer packaging, and mold shrinkage before cutting steel.
We overmold LSR and HCR onto customer-supplied inserts made strictly of polycarbonate (PC), polypropylene (PP), polyamide (PA), stainless steel, aluminum, and copper using controlled primer adhesion on every substrate.
Free 3D-printed samples (1–3 pcs, shipping paid by customer once requirements, quote, and drawings are confirmed) verify rigid assembly fit and groove alignment. Durometer feel, seal compression set, valve cracking pressure, and disinfection compatibility require T1 molded silicone samples (typically 7–15 days).
B2B Factory Direct · 24h Engineering & Tooling Review
Send 2D/3D CAD files, mating housing details, contact/cleaning conditions, and required quality documents for an engineering response within 24 hours.