
Youbang · B2B Custom Silicone Manufacturing · Dongguan
Liquid Silicone Injection Molding (LSR)
Closed-loop two-part platinum LSR metering and injection on 85T and 120T presses in Dongguan—engineered for thin membranes (0.25–0.30 mm), micro-vent pinholes, clean parting shut-offs, and repeatable multi-SKU durometer runs.
- 1Sealed A + B drums
- Two liquid silicone components remain separated in sealed containers to prevent premature crosslinking.
- 21:1 metering & pigment dosing
- Positive-displacement pumps meter A, B, and liquid color masterbatch through a static mixer without open-mill dust exposure.
- 3Heated precision steel cavity
- Low-viscosity LSR fills thin walls, micro-pins, and complex undercuts before rapid platinum addition curing.
- 4Post-curing & clean packing
- Demolded parts undergo ventilated oven post-curing (typically 200 °C × 4 h) and enter our 150–200 m² clean washing/packing zone when required.
Equipment: 2 LSR injection molding machines (85T & 120T)
Wall thickness: 0.25 mm min / 0.30 mm stable mass production (per part)
Precision tolerance: typically ±0.05 mm on critical features (±0.1–0.2 mm standard)
Sampling & lead time: new mold T1 typically 7–15 days; mass production 15–30 days
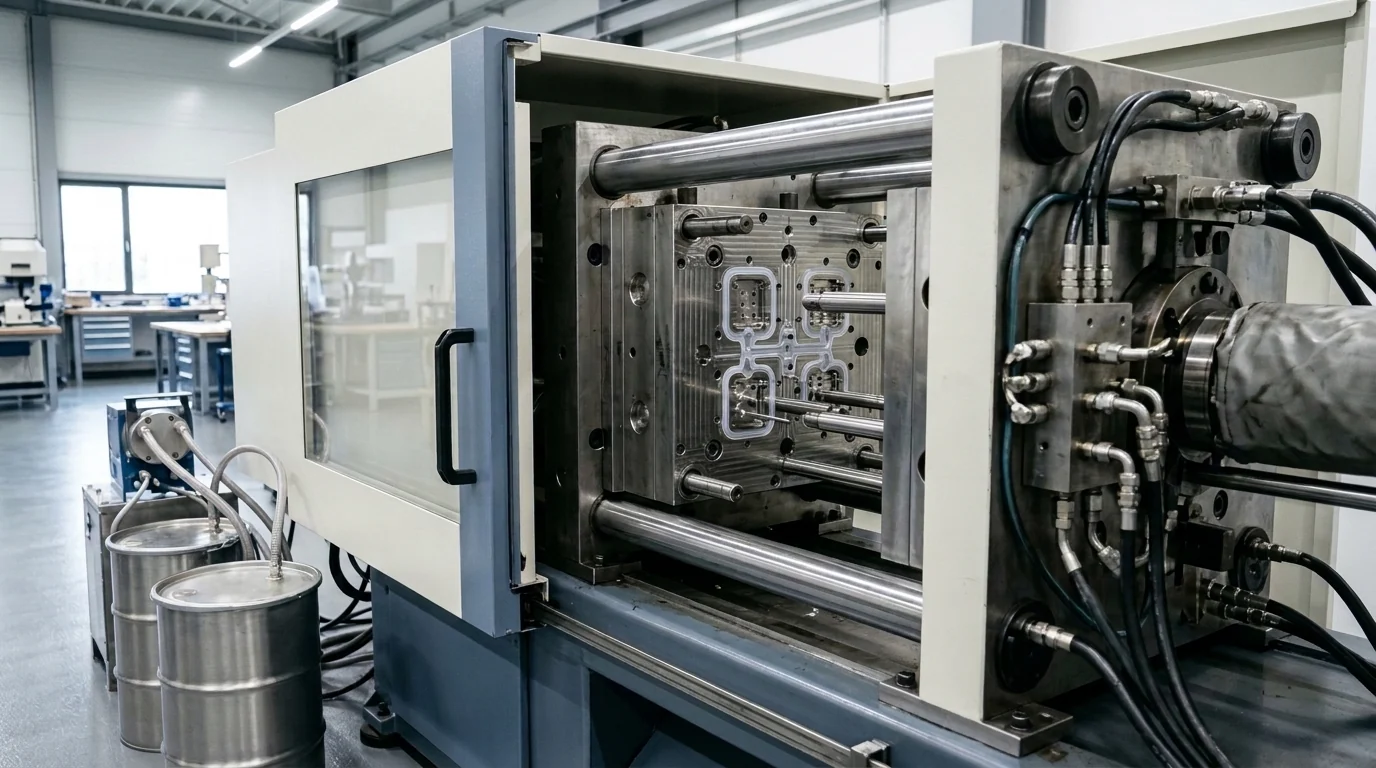
Four DFM checkpoints to mark on your LSR drawing
Convert functional targets into verifiable steel shut-offs, gate locations, and metrology datums before cutting mold steel.
- Thin membranes & wall transitions (0.25–0.30 mm)
- Highlight membranes, umbrella valves, or bell walls approaching 0.25–0.30 mm and smooth out abrupt thick-to-thin steps to prevent air traps and knit lines.
- Gate witness & cold/open runner zone
- Define non-sealing, non-cosmetic zones where a micro-gate vestige (pinpoint, submarine, or edge gate) is permissible without interfering with mating parts.
- Parting shut-off & micro-vent features
- Specify sealing lips, mucosal-contact rims (such as menstrual cups), and molded-in vent holes so precision steel shut-offs eliminate secondary punching.
- Platinum LSR grade, Shore A & volatile limits
- Specify target hardness (0–80 Shore A; commonly 30–70A), elastomer brand preference (Wacker, Shin-Etsu, Momentive, Dow, Elkem, Dongjue, Zheng'an), and FDA/LFGB/ISO 10993 test scope.
Capability figures depend on part geometry, flow-length-to-wall ratio, and elastomer grade; final tolerances are confirmed during pre-tooling DFM review.
Structured T1 first-article validation
Before approving mass production, we align T1 molded silicone samples against your 2D inspection drawing, post-curing spec, and functional assembly checks.
- Verify critical dimensions on our 2D optical coordinate measuring system and hardness across 3 Shore A durometers.
- Inspect parting-line flash, gate vestige height, and pinhole clearance under illuminated magnification.
- Log ventilated oven post-curing (typically 200 °C × 4 h; ≤ 0.5% volatile weight loss for LFGB/baby/intimate care) and link raw-material lot to shipment ID.
- Confirm geometry early with a free 3D-printed prototype (1–3 pcs on confirmed quote & CAD; shipping by buyer) before committing to steel machining.
Which route fits the project?
Moderate batch volume with thicker walls (≥ 0.50 mm)?
Compare 200–250T HCR compression molding when lower upfront tooling investment outweighs LSR automation and ultra-thin-wall requirements.
Compare HCR compression molding →Bonding LSR onto PC, PA, PP, or metal inserts?
Review substrate heat resistance, mechanical interlocks, and primer application boundaries for customer-supplied plastic or metal hardware.
Review insert overmolding →Sourcing & Tooling FAQ
Key Answers Before Tooling
Covering CAD readiness, custom MOQ evaluation, free 3D fit checks vs. T1 silicone samples, NDA protection and mold ownership.
Send your drawing or sample photo directly to Zhou Li’s engineering desk for a 24h DFM reply.
At what annual volume or part geometry does LSR injection beat HCR compression?+
LSR injection is typically preferred when geometry demands ultra-thin walls (0.25–0.30 mm), molded-in micro-pinholes, flash-sensitive mucosal or fluid-sealing rims, or high annual volumes (often 20,000–100,000+ pcs/year) where shorter cycle times offset higher precision mold investment.
Can one LSR steel mold run multiple Shore A hardnesses (e.g., 35A Soft and 45A Classic)?+
Frequently yes across adjacent platinum LSR grades (such as 35A and 45A menstrual cups or valves), because linear shrinkage shifts only slightly. We test both durometers during T1/T2 sampling to verify dimensional tolerances before locking specifications.
Do you mold LSR inside a certified cleanroom?+
Molding takes place in our dedicated LSR injection shop (85T and 120T presses) using closed-barrel A/B liquid feed. After ventilated oven post-curing, medical and personal-care silicone components are washed, inspected, assembled, and sealed inside our 150–200 m² clean assembly and packaging area under ISO 13485:2016 (62026Q00072R100) batch traceability.
Who owns the LSR injection mold once paid for?+
Customer-funded molds belong 100% to the customer. Youbang provides free routine maintenance and in-plant storage during active production (contacting you first if a tool sits inactive for 2 consecutive years), and signs NDAs prior to CAD exchange.
B2B Factory Direct · 24h Engineering & Tooling Review
Submit your 3D CAD for an LSR DFM & tooling review
Share STEP/IGES + 2D PDF drawings, Shore A target, destination compliance standards, and batch forecast. We respond within 24 hours with gating, parting, and quotation feedback.
Direct Dongguan Engineering Desk
- Accepts STEP / IGES / PDF / DWG or sample photos
- New mold T1 typically 7–15 days · Mass run 15–30 days
- Direct Tel / WeChat: +86 185 6655 6911 (Zhou Li)