
Key Sourcing Takeaways
- Anchor quality system audits on verified registration scope: Dongguan Youbang holds ISO 13485:2016 (Certificate No. 62026Q00072R100, production of silicone products excluding products requiring qualification licensing) alongside ISO 9001:2015 (21424Q0270R1S).
- Require four factory-issued per-lot deliverables from 100 pcs upward: upstream elastomer Certificate of Analysis (CoA) & lot number, closed-loop LSR A/B + 200 °C × 4–6 hours post-cure shop log, 2D optical First Article Inspection (FAI), and 36-month physical sample retain archiving.
- Separate factory batch traceability from finished-device regulatory ownership: Youbang coordinates ~10-day third-party ISO 10993 / FDA / LFGB lab testing via SGS, Intertek, or TÜV on actual molded components, while finished medical-device registration and market licensing remain with the brand owner.
Four-Tier ISO 13485 Batch Traceability & Lab Documentation Flow
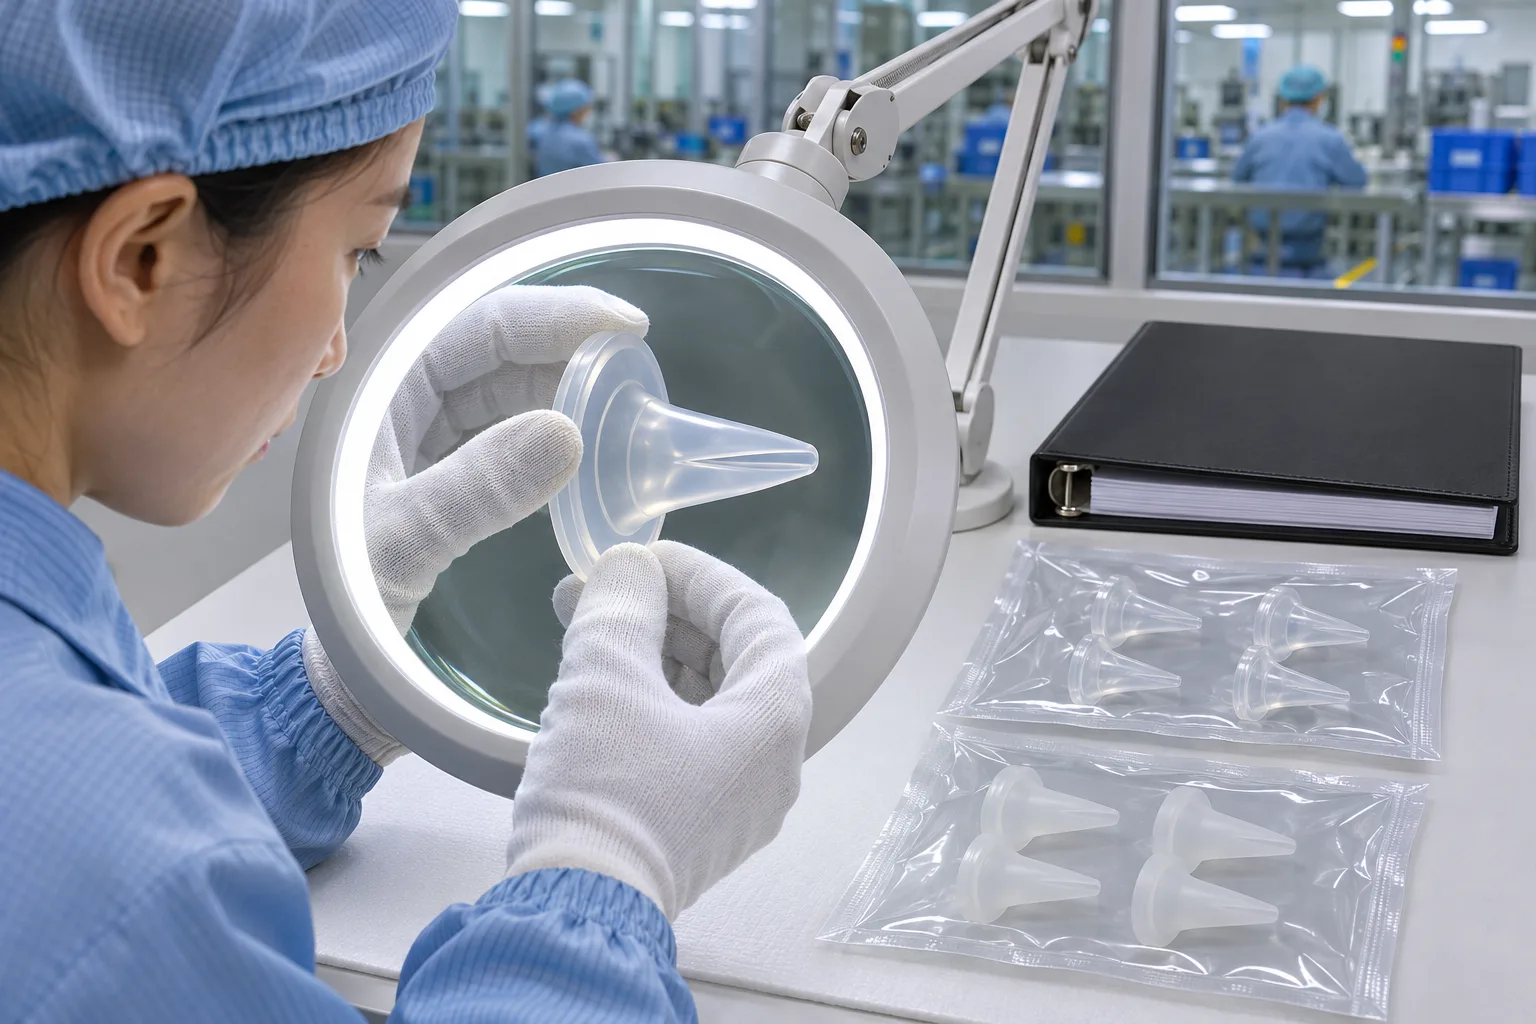
Procurement engineers sourcing external respiratory cushions, diagnostic cartridge seals, menstrual cups, or fluid-control duckbill valves rarely reject a vendor over injection cycle times—audits stall when quality teams discover gaps between paper certificates and lot-level component traceability. Knowing exactly which documents belong inside the molding factory's folder versus third-party labs keeps compliance timelines on schedule.
Inside Dongguan Youbang's 8,000 m² Dongguan plant (operating 10 closed-loop LSR presses 85T–160T, 6 circulating post-cure ovens, 2D optical metrology, and our 600 m² air-showered wash & double-PE pack zone), buyer audit dossiers organize into four clear layers.
1. Four-Tier Traceability Dossier vs. Ownership Boundaries
Match component evidence directly to lot numbers, exact equipment logs, and finished molded parts—never rely on generic supplier brochures. All quality records remain archived for 36 months from 100 pcs pilot runs through ongoing volume.
| Audit Dossier Tier | Exact Documents & Data Logged | Origin & Custody Owner | Why QA Auditors Check This Item |
|---|---|---|---|
| Tier 1 · Verified System Scope | ISO 13485:2016 (62026Q00072R100) & ISO 9001:2015 (21424Q0270R1S) PDFs + entity verification (8,000 m² plant) |
Youbang QMS (on Certificates page) | Proves controlled production management while clearly confirming finished-device licensing stays outside contract molding |
| Tier 2 · Raw Elastomer & Insert Traceability | Upstream platinum A/B LSR CoA batch numbers (Wacker, Shin-Etsu, Momentive, Dow, Elkem) + buyer insert batch specs |
Raw elastomer vendor -> Youbang intake log | Links every lot back to catalyst purity, peroxide-free status, RoHS/REACH compliance & substrate resin grade |
| Tier 3 · Shop-Floor Lot & FAI Records | Press tonnage/temp record, 200 °C × 4–6 hours bake curve log, Shore A readings, 2D optical FAI (±0.05 mm critical datums) & 600 m² double-PE pack lot |
Youbang Production & Metrology QA | Demonstrates zero-skip thermal conditioning, repeatable cross-section tolerances & contamination-free wash/seal isolation |
| Tier 4 · Finished-Part Biocompatibility & Filing | Component-level ISO 10993 (cytotoxicity/irritation/sensitization), FDA 21 CFR 177.2600, or LFGB (~10 days via SGS/Intertek/TÜV) |
Third-party lab coordinated by Youbang; brand owner owns registration | Validates finished molded, baked, pigmented/overmolded components match target clinical or personal-care exposure rules |
2. Clean 600 m² Isolation Without Inflated Cleanroom Claims
Transparency protects your audit team from unpleasant surprises during remote or on-site inspections:
- What Youbang Operates Inside
600 m²: Dedicated post-molding purified ultrasonic washing tanks, backlit burr/lint visual inspection benches, assembly tables, and double-PE thermal bag sealing behind air-showered gowning buffers—paired with closed-loop A/B LSR metering cylinders that keep raw platinum rubber sealed inside hoses prior to heated cavity curing. - No Unverified ISO Class Claim: Unless a buyer sponsors dedicated room certification for a specific sub-enclosure, Youbang intentionally documents actual physical controls (wash tanks, double-PE pouches, lot separation, backlit checks) without inflating claims.
3. Aligning T1 Samples with Pre-Market Lab Submissions
Smart hardware & personal-care launches run physical T1 fit approval and lab testing cleanly in sequence:
- Validate free 3D geometry prints on housing cradles (
buyer covers freight). - Approve molded T1 platinum LSR parts (
7–15 days) for dimensional optical FAI and Shore A/peel integrity. - Submit locked T1/pilot parts (
from 100 pcsbatches baked200 °C × 4–6 hours) straight to SGS, Intertek, or TÜV (~10 days) for targetISO 10993or food/mucosal compliance reports ahead of brand regulatory submission.
Review full verified factory certificates & quality control scope or inspect our LSR medical & external device component molding line for a first engineering reply within 24 hours.