
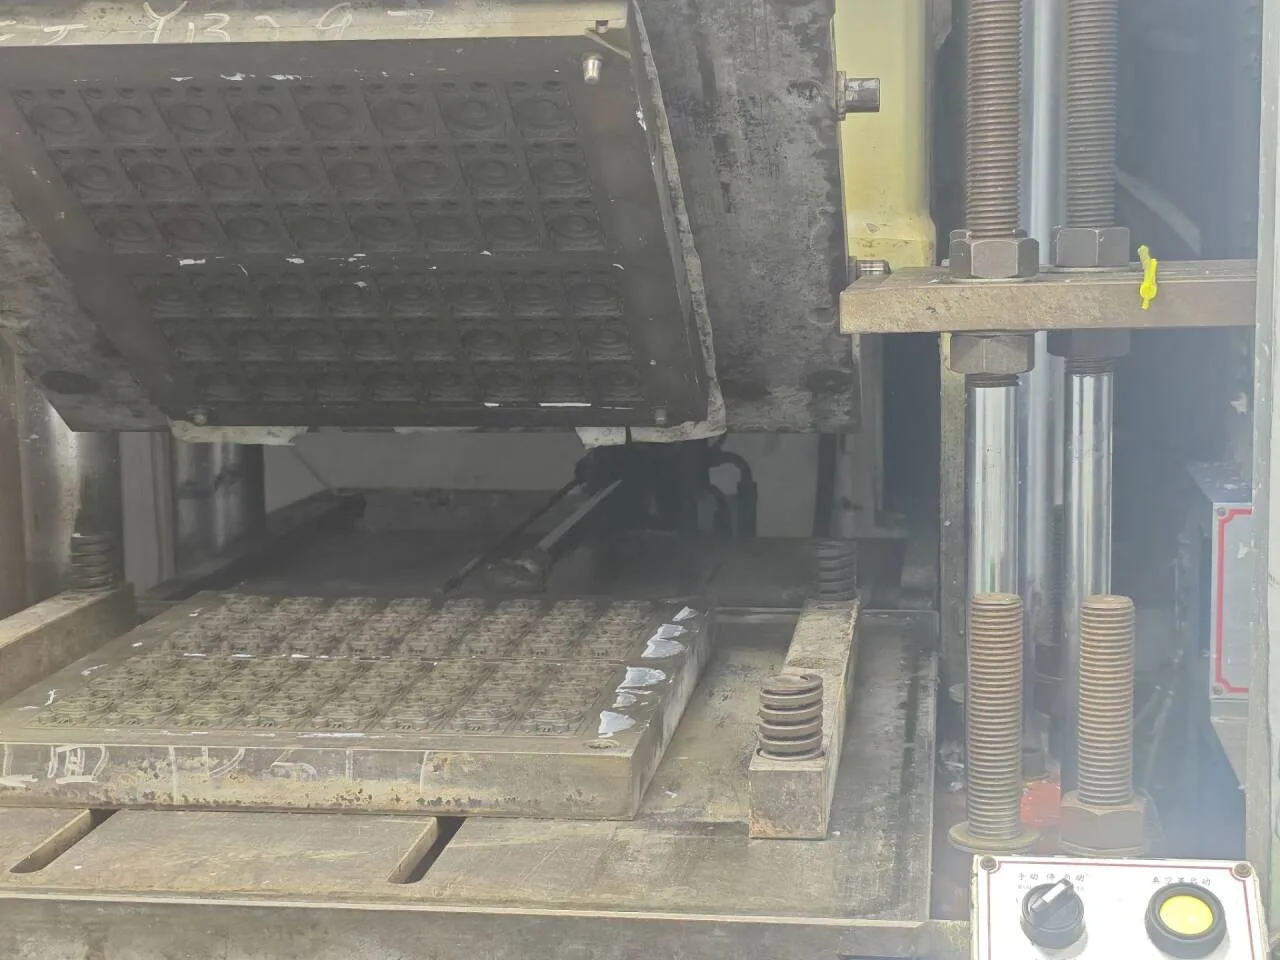
Geometry & interfaces
Review micro-bristle cleansing heads and sonic-device sealing sleeves, mating parts and loaded sections before fixing tool cavities.
Explore molding routesYoubang · B2B Custom Silicone Manufacturing · Dongguan
Develop micro-bristle cleansing heads and sonic-device sealing sleeves to your drawings. Start with mating geometry, use conditions and a molded-sample acceptance plan at our 8,000 m² Dongguan factory.
Review micro-bristle cleansing heads and sonic-device sealing sleeves, mating parts and loaded sections before fixing tool cavities.
Explore molding routes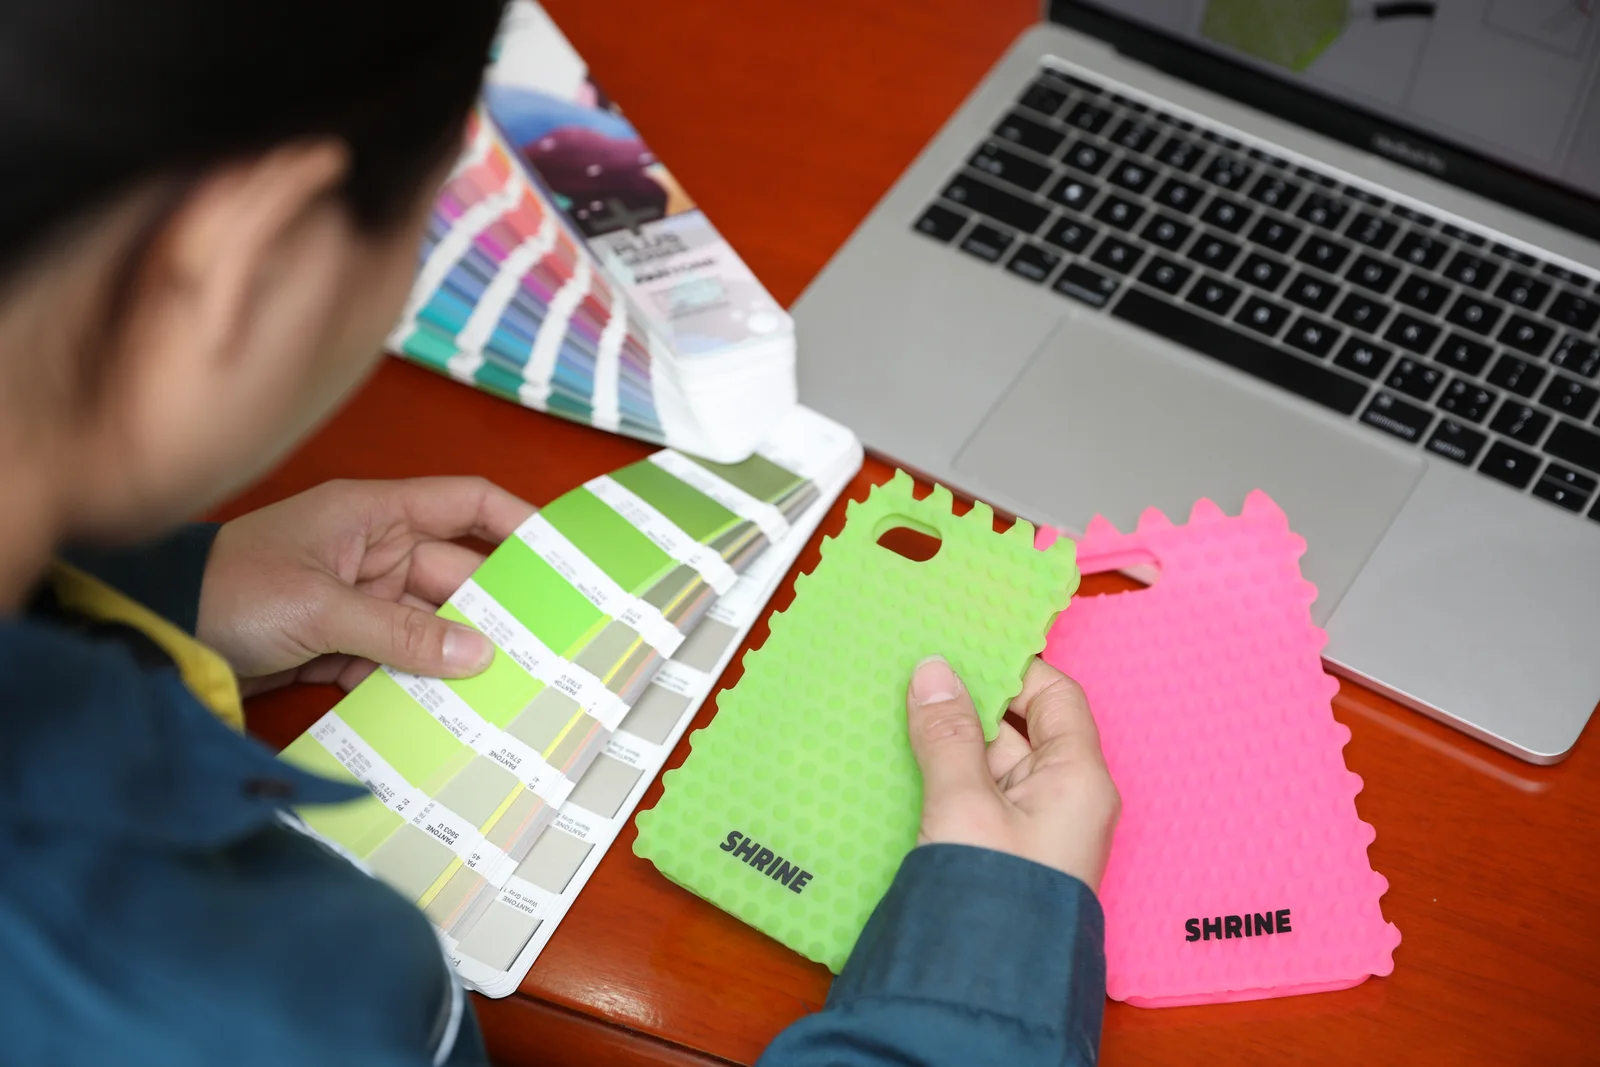
Approve molded texture, color and handling with the intended contact media and packaging.
Review finish & packagingLocation, attachment and cleaning change the interface to be reviewed.
Provide tip radius, length and spacing; use a test patch to assess fill and demolding before the full tool.
Supply shell resin, datum, button travel and charging-port geometry, with production shells for bond trials.
Define cleanser, exposure cycles and the assembly water test; approve the actual sealed device.
Define test scope from destination market, contact duration and cleaning conditions.
For micro-bristle cleansing heads and sonic-device sealing sleeves, identify critical interfaces and functional tests on the drawing. Retain the molded approval sample and record inspection conditions before repeat orders.
Sourcing & Tooling FAQ
Covering CAD readiness, 100 pc trial & 1,000 pc / $2,000 USD standard MOQ policy, free 3D fit prototypes vs. T1 silicone samples, NDA protection, and mold ownership.
Send your drawing or sample photo directly to Youbang’s engineering desk; we send an initial response within 24 hours.
Flow length, spacing and demolding strain interact. Compare a bristle test patch before tooling the whole head; do not extrapolate a general LSR wall minimum to unsupported bristle tips.
Review compound hardness and bristle aspect ratio independently. Use molded comparison patches with the intended cleanser to separate material softness from geometric bending stiffness.
No. Water ingress depends on the assembled housing, buttons, seams and charging connection. Agree an assembly-level test plan and inspect seals after vibration and cleaning cycles.
Map travel, actuation force and hard-stop clearance against the switch. T1 checks should include off-center pressing and repeated flexing, not only static membrane thickness.
Review shell resin, heat resistance and bond preparation first. Provide representative production shells; prototype resin or paint can bond differently and hide production delamination risk.
Approve bristle completeness, tip appearance, vibration feel, port fit and cleaning performance on molded assemblies. Keep a sealed reference sample and define the inspection method for damaged or missing tips.
B2B Factory Direct · initial response within 24 hours
Send bristle length and spacing, device shell resin and port geometry with the cleaning and assembly ingress test plan.