
Custom Silicone Case Study · Personal Care Devices · 0.6 mm EDM Bristle Array & PC Core LSR

Molding Uniform 0.6 mm Tapered LSR Bristle Arrays Over a Waterproof PC Core

Developing a sonic facial cleanser silicone sleeve across Dongguan Youbang's 5-axis EDM toolroom and 85T–160T closed-loop LSR lines—solving micro-hole air trapping at 0.6 mm bristle tips while sealing customer-supplied polycarbonate (PC) or polyamide (PA) inner motor cores cleanly with baked silane primer and 200 °C × 4–6h post-curing from 100-pc pilot runs.

Molding Uniform 0.6 mm Tapered LSR Bristle Arrays Over a Waterproof PC Core
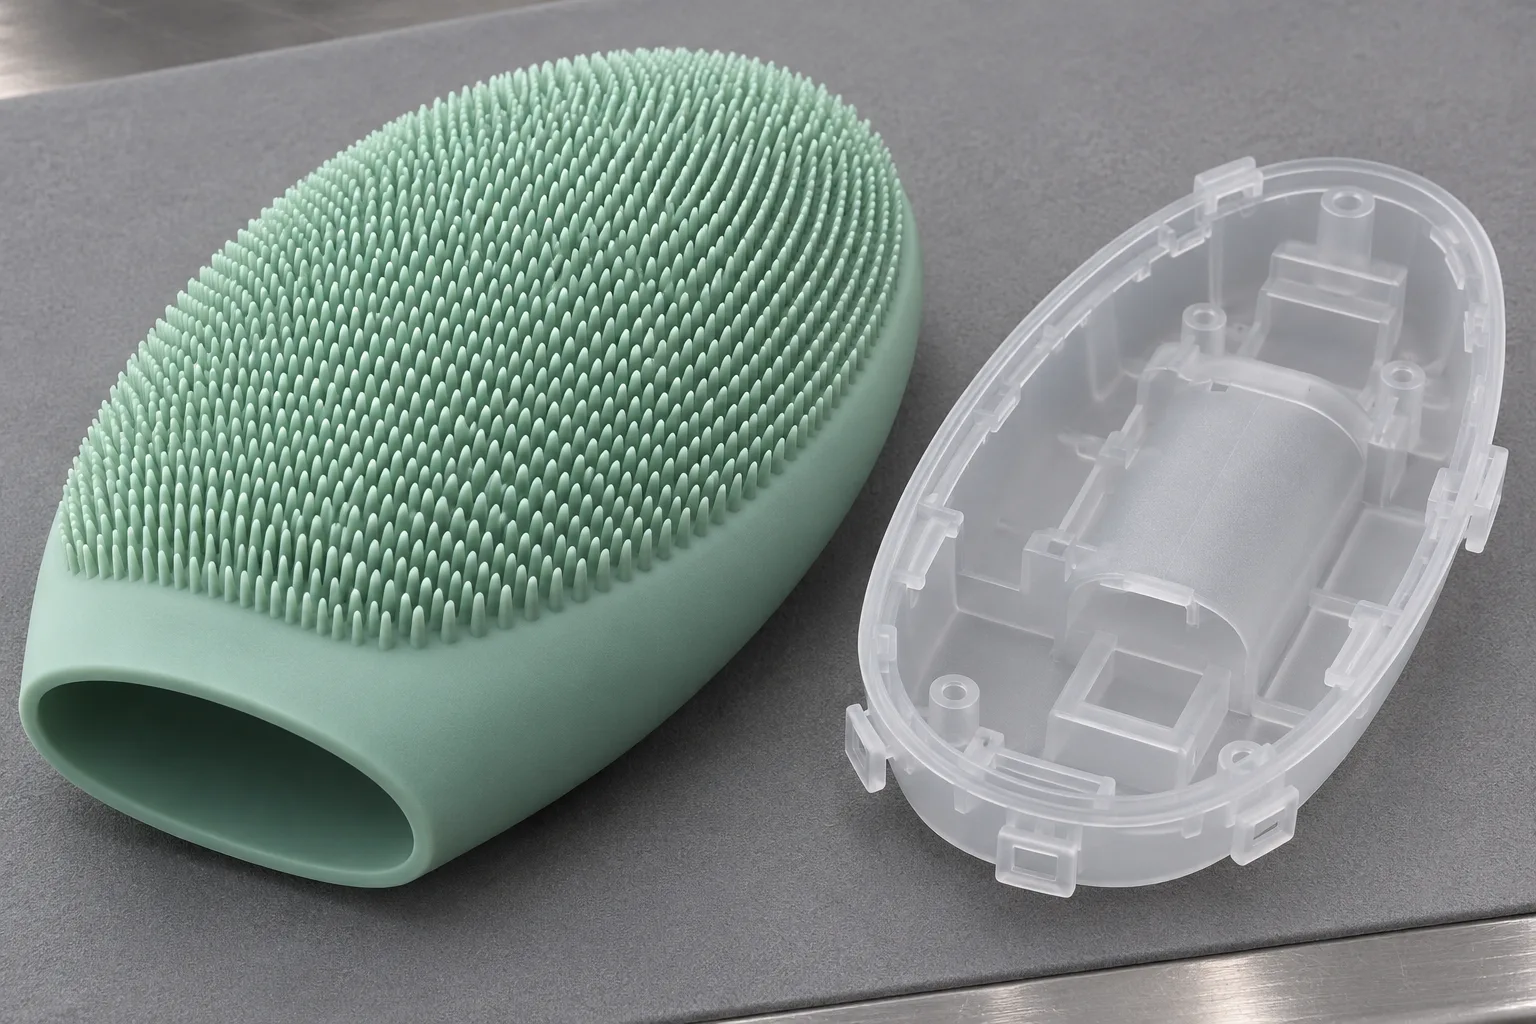
Matte pastel sage-teal molded LSR ultrasonic facial cleanser sleeve showing uniform 0.6 mm tapered bristles beside its rigid frosted polycarbonate inner motor shell
Micro-Cavity Tooling5-Axis Fine EDM + Vacuum LSR Venting
Bristle Tip Spec0.6 mm Tapered Array · Zero Air Trap
Core Waterproof SealBuyer PC / PA Insert + Silane Primer
Cure & Pilot Entry200 °C × 4–6h Bake · 100 pcs Trial Ready
Before Tooling

Eliminating Short-Shot Stubby Bristles, Flash Webbing & Charging-Port Waterproof Seepage

Hundreds of dense 0.6 mm micro-holes lock trapped air instantaneously when fast-shooting LSR floods across shallow gate faces, resulting in bald cropped tips—while sloppy inner core overmolding lets shower soap seep past charging collars straight onto sonic motors.

  • Evacuate trapped air across hundreds of sub-millimeter bristle holes so every single soft tip fills to uniform tapered height without high-pressure parting flash.
  • Maintain zero sticky tack across sensitive facial silicone surfaces using non-oily cured surface finishes that dry rapidly between washes.
  • Seal buyer-supplied PC/PA inner vibration housings along stepped waterproof collar beads capable of cohesive tear bonding after detergent thermal cycles.
Sample Approval

Full Velvet Bristle Tips, Submersible Housing Seal & Multi-Shade Launch Scaling

T1 brush bodies delivered smooth uniform 0.6 mm bristles without bent or stubby zones, passed warm-soapy wash & waterproof immersion seal checks over supplied PC cores, and moved straight from 100-pc colorway validations into 85T–160T closed-loop replenishment.

  • Optical backlit bristle height uniformity checks across dense 0.6 mm coarse and gentle facial zones.
  • Cohesive rubber-tear pull verification and warm soapy water waterproof collar records over buyer PC/PA cores.
  • 36-month platinum LSR compound CoA & Pantone batch archiving alongside 100% buyer-owned steel mold storage.

Tooling and Process Steps

Precision EDM Copper-Electrode Arrays, Vacuum Cavity Venting & Baked Core Overmolding

Tooling engineers drilled matched micro-vented EDM cavities sized for low-viscosity platinum LSR, paired with controlled customer-insert primer baking and stepped seal shutoffs.

01

High-Precision 5-Axis Copper-Electrode EDM Array & Periphery Air Escape

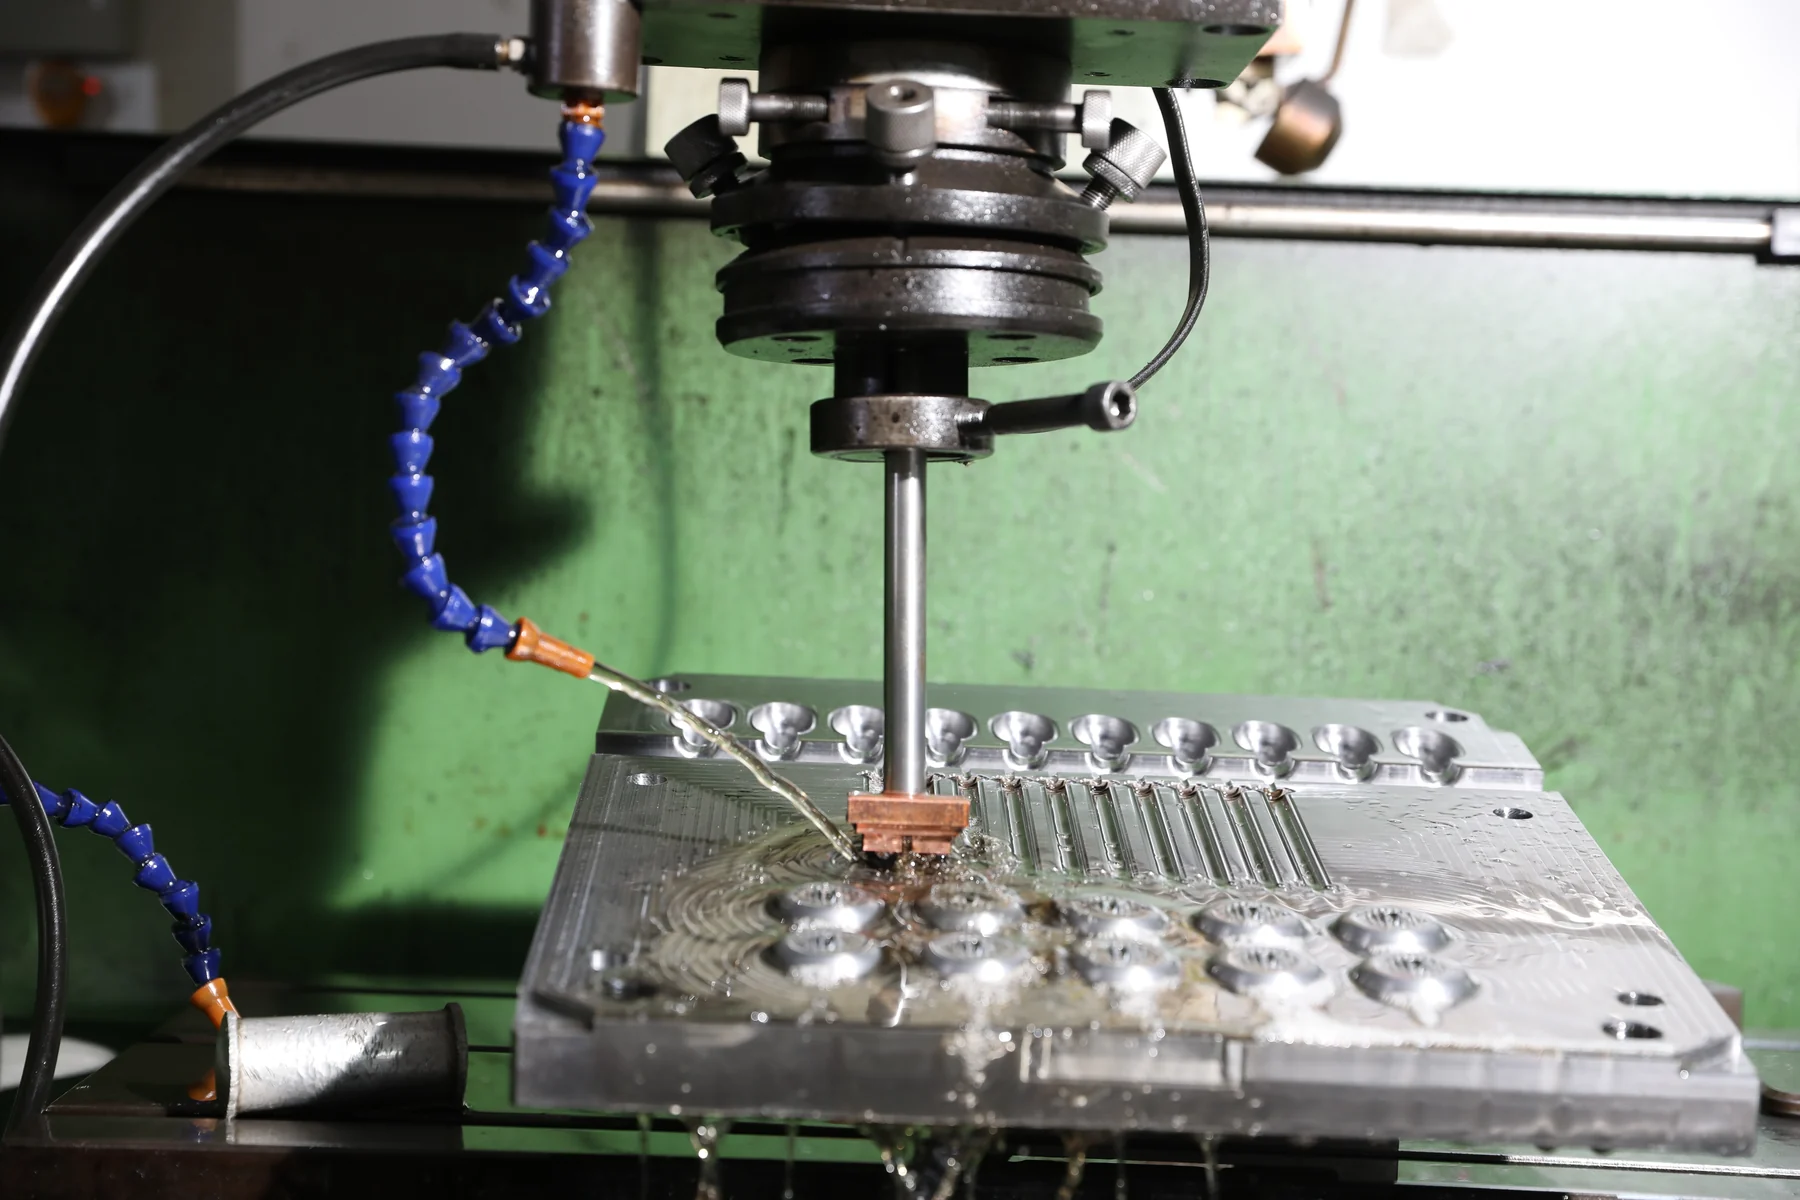
Machined multi-diameter 0.6 mm tapered micro-cavities via controlled 5-axis EDM spark erosion with micro-ground perimeter evacuation vents (±0.05 mm shutoff lands), letting injected A+B LSR vent cleanly to tip crowns without tip burns or ragged flash webbing.

02

Customer PC / PA Housing Pre-Bake, Silane Primer & Collar Lip Shutoff

Pre-dried customer-supplied rigid polycarbonate (PC) or polyamide (PA) inner housings, applied skin-safe industrial silane primer along sealed bonding grooves, and centered cores inside stepped LSR mold seats so charging recesses stay completely burr-free.

03

200 °C × 4–6h Post-Cure, 600 m² Wash & Backlit Tip-Height FAI Checks

Conditioned demolded sleeves at 200 °C × 4–6 hours across 6 circulating ovens (keeping volatiles ≤0.5%), ultrasonic washed and backlit-inspected bristle fullness inside our 600 m² clean zone, and checked waterproof core peel resistance across T1 batches.

Precision EDM Copper-Electrode Arrays, Vacuum Cavity Venting & Baked Core Overmolding
In-house EDM spark-erosion & CNC steel mold cavity machining

B2B Factory Direct · initial response within 24 hours

Share Cleansing Brush Outer STEP & Rigid PC/PA Housing Drawing

Upload tapered bristle zone maps, supplied PC/PA core housing tolerances, and target Pantone shades for an initial tooling reply within 24 hours.

✓ Trial from 100 pcs · Standard 1,000 pcs or $2,000 USD✓ Free 3D-printed fit prototypes before steel tooling✓ Paid molds 100% owned by customer
View helpful RFQ inputs
  • Silicone outer brush 3D STEP + buyer polycarbonate (PC) / PA core CAD
  • Bristle diameter/pitch targets (e.g., 0.6 mm) & desired 35–50A bristle feel
  • IP waterproof immersion target & pilot trial quantity (from 100 pcs)

Send Your Project Brief or CAD

For confidential drawings, sign the mutual NDA before uploading the files.

Only rights holders or their authorized representatives may upload files. We keep inquiries and attachments to prepare quotes and follow up on your project.

Prefer email or files > 20 MB? Send directly to zhouli@ybsilicone.com · Privacy Policy