
Custom Silicone Case Study · Cookware OEM · PA66 Rigid Insert Overmolding

Seamless PA66 Nylon Core Spatula Encapsulation Without Oil-Soak Delamination

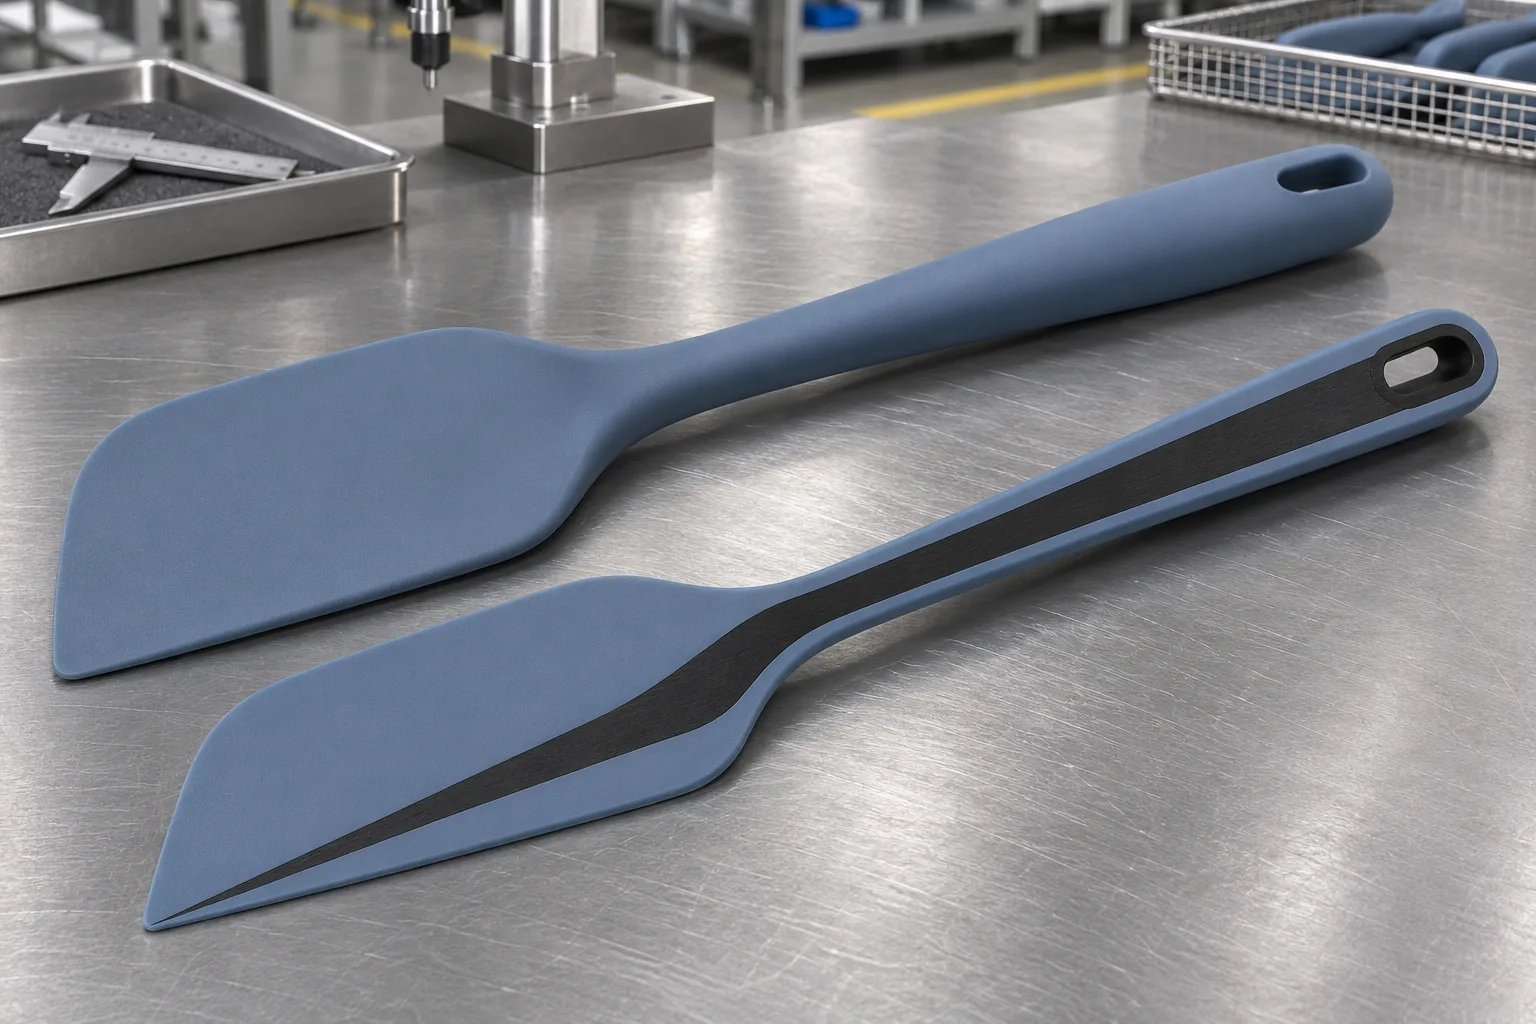
Developing an ergonomic two-edge silicone kitchen spatula molded cleanly around a buyer-supplied glass-filled PA66 nylon stiffener spine—eliminating trapped moisture steam blisters, hiding core locating marks seamlessly, and passing 200 °C hot oil soak checks with 0.8 mm feathered pan-scraping blades from 100-pc pilot runs.

Seamless PA66 Nylon Core Spatula Encapsulation Without Oil-Soak Delamination
Slate-blue silicone overmolded spatulas beside a raw glass-filled PA66 nylon stiffener core and sectioned sample showing full elastomer bonding
Molding Process200T–350T HCR + PA66 Insert Priming
Bond & Hygiene RulePre-Baked Core · Food-Contact Primer
Scraping Tip Profile0.8 mm Tapered Lip · ±0.05 mm Core Pin Fit
Cure & Pilot Entry200 °C × 4–6h Post-Cure · 100 pcs Trial
Before Tooling

Stopping Hydrolysis Delamination, Off-Center Insert Show-Through & Thick Neck Sag

Full-encapsulated nylon-core spatulas fail rapidly in the field when absorbed PA66 nylon moisture blisters rubber during high-temp compression, unsupported cores drift sideways under molding pressure leaving bare black plastic exposed on one face, or primer washes off after repeated hot oil stir-frying.

  • Drive out hygroscopic PA66 nylon moisture ahead of priming and compression molding so zero steam pockets inflate bubbles beneath silicone skins.
  • Center rigid inserts cleanly across thin tapered blade zones without thick ugly parting scars or core shift exposure.
  • Maintain firm neck stirring stiffness while tapering leading scraping edges down to 0.8 mm flexible silicone for non-stick pan wiping.
Sample Approval

Crisp Tapered Edge Flexibility, Zero Blistering & Cohesive 100-Pc Launch

T1 overmolded spatulas wipe glass bowls clean along feathered 0.8 mm blade tips while resisting neck bend during thick batter mixing, pass optical thickness/balance inspections, and advance directly from 100-pc retail pilot runs into coordinated color collections.

  • Hot cooking-oil immersion & dishwasher thermal cycle peel-test records confirming cohesive rubber bond over buyer PA66 cores.
  • T1 tapered tip cross-section gauge checks (0.8 mm scraping rim; balanced silicone encapsulation thickness across paddle neck).
  • 36-month master platinum compound & primer batch retention archive plus free maintenance on the 100% buyer-owned steel mold.

Tooling and Process Steps

Core Pre-Drying, Silane Primer Cure & Stepped Sacrificial Pin Localization

Rather than resorting to noisy exposed-seam two-piece sleeves, engineers paired controlled core pre-conditioning, uniform baked silane primer coating, and precision stepped locating pins inside split 5-axis steel cavities.

01

Customer PA66 Insert Pre-Baking & Clean Silane Primer Application

Pre-dried incoming customer-supplied glass-filled PA66 stiffeners prior to degreasing and dipping/baking food-contact silane primer—forming strong chemical bond affinity capable of resisting hot water, dishwasher steam, and 200 °C frying oil exposure.

02

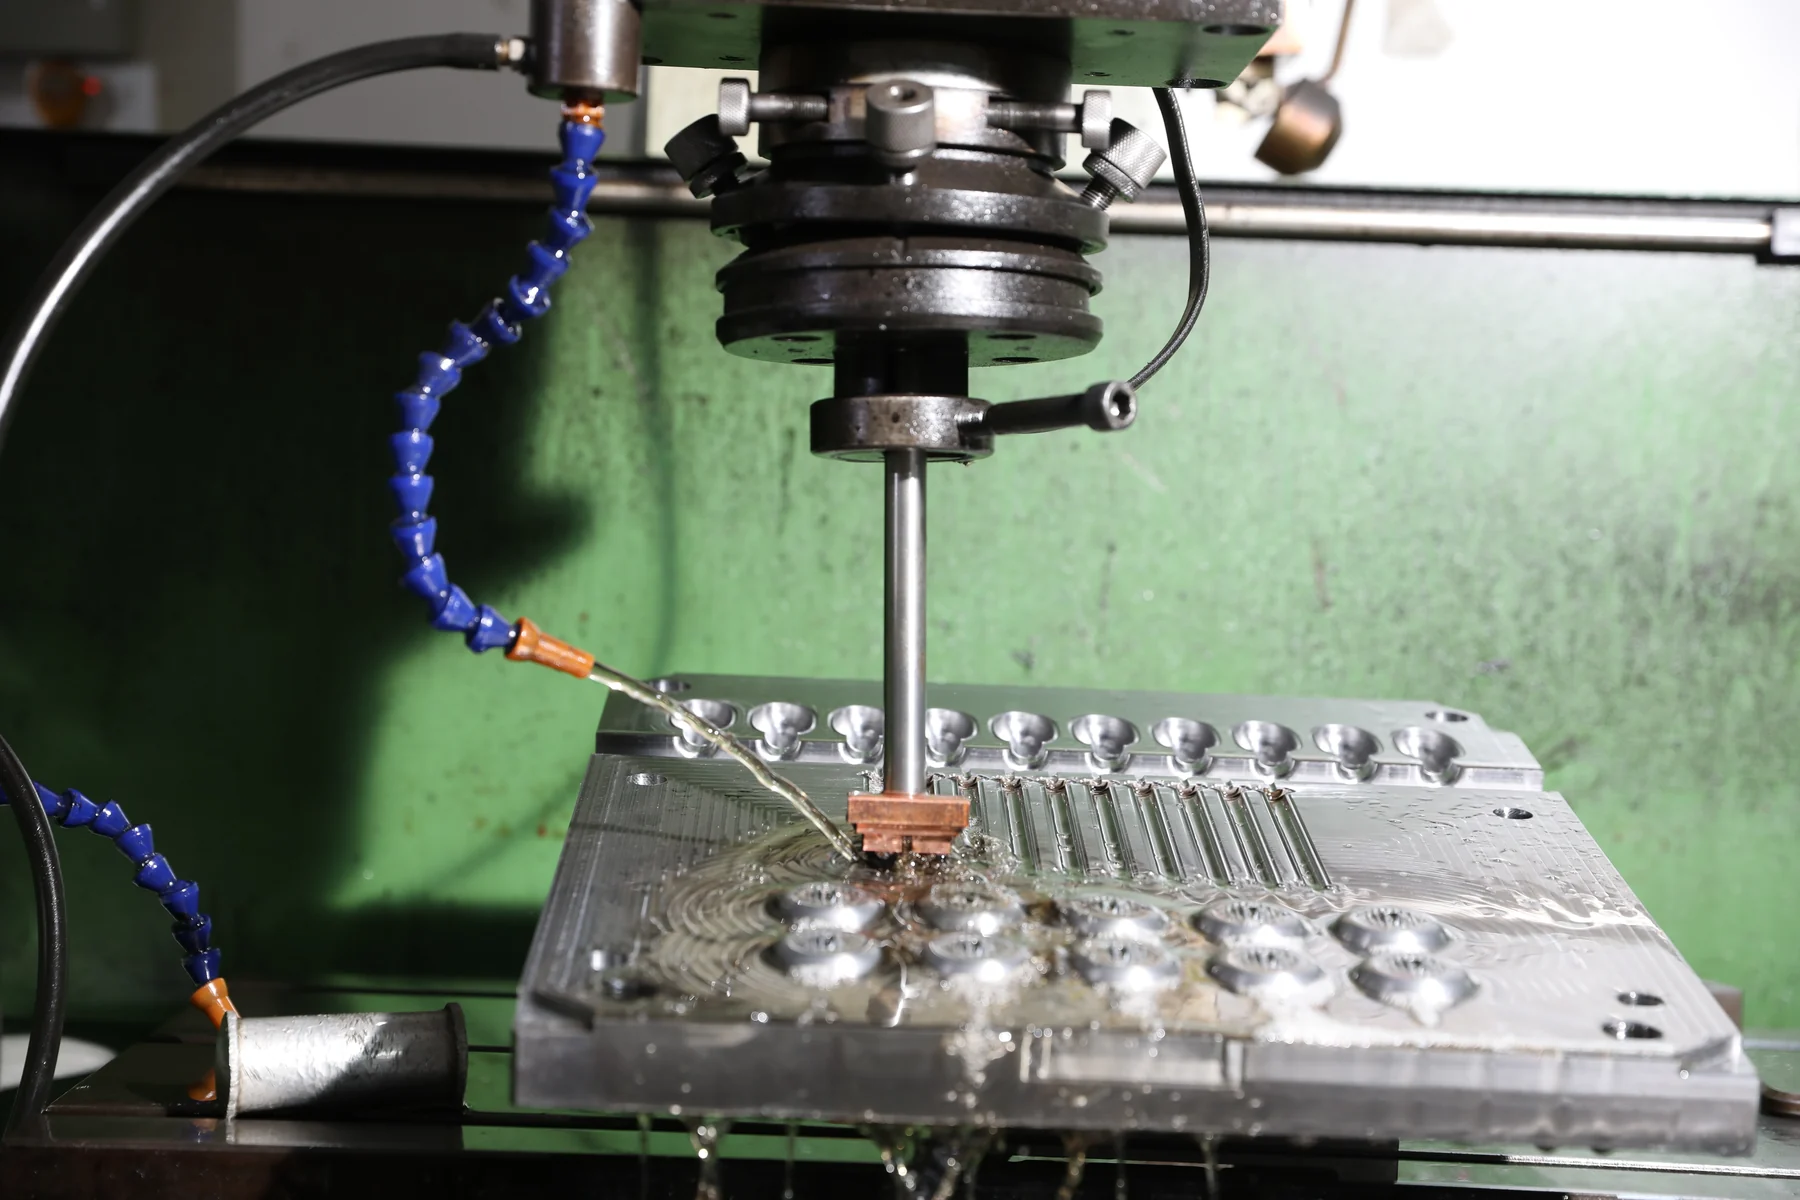
Opposing Balanced Pin Support Inside 5-Axis HCR Cavity Shutoffs

Machined flush micro-retaining recesses (±0.05 mm pin alignment) locking the nylon neck rigid under cavity compression pressure, keeping silicone wall coverage symmetrical down both faces of the paddle neck without show-through.

03

Platinum Elastomer Compression, 200 °C × 4–6h Post-Cure & Oil-Boil Peel Test

Compression-molded 55A matte platinum silicone over the primed core, baked finished spatulas for 200 °C × 4–6 hours across 6 circulating ovens, and performed hot-oil / boiling soak tear checks confirming cohesive rubber tearing rather than bare nylon release.

Core Pre-Drying, Silane Primer Cure & Stepped Sacrificial Pin Localization
In-house EDM spark-erosion & CNC steel mold cavity machining

B2B Factory Direct · initial response within 24 hours

Upload Utensil Outer STEP & Customer Nylon / Steel Core Drawing

Share paddle geometry, rigid core material grade (PA66, stainless steel, aluminum), and target color splits for a first engineering reply within 24 hours.

✓ Trial from 100 pcs · Standard 1,000 pcs or $2,000 USD✓ Free 3D-printed fit prototypes before steel tooling✓ Paid molds 100% owned by customer
View helpful RFQ inputs
  • Outer silicone spatula 3D STEP + supplied PA66 nylon / stainless core CAD
  • Operating oil/dishwashing temp expectations & FDA / LFGB test targets
  • Pilot run volume (supported from 100 pcs) & bundle colorway plan

Send Your Project Brief or CAD

For confidential drawings, sign the mutual NDA before uploading the files.

Only rights holders or their authorized representatives may upload files. We keep inquiries and attachments to prepare quotes and follow up on your project.

Prefer email or files > 20 MB? Send directly to zhouli@ybsilicone.com · Privacy Policy