
Representative Engineering Program · Medical Components · LSR Insert Overmolding

Precision Dual-Lip LSR Gasket Overmolded onto a Customer-Supplied PC Diagnostic Frame

Replacing error-prone manual O-ring seating on a European non-implantable bedside monitoring cartridge—combining 85T/120T low-pressure LSR injection overmolding, controlled silane primer treatment, and mechanical shutoff interlocks under ISO 13485 traceability.

Precision Dual-Lip LSR Gasket Overmolded onto a Customer-Supplied PC Diagnostic Frame
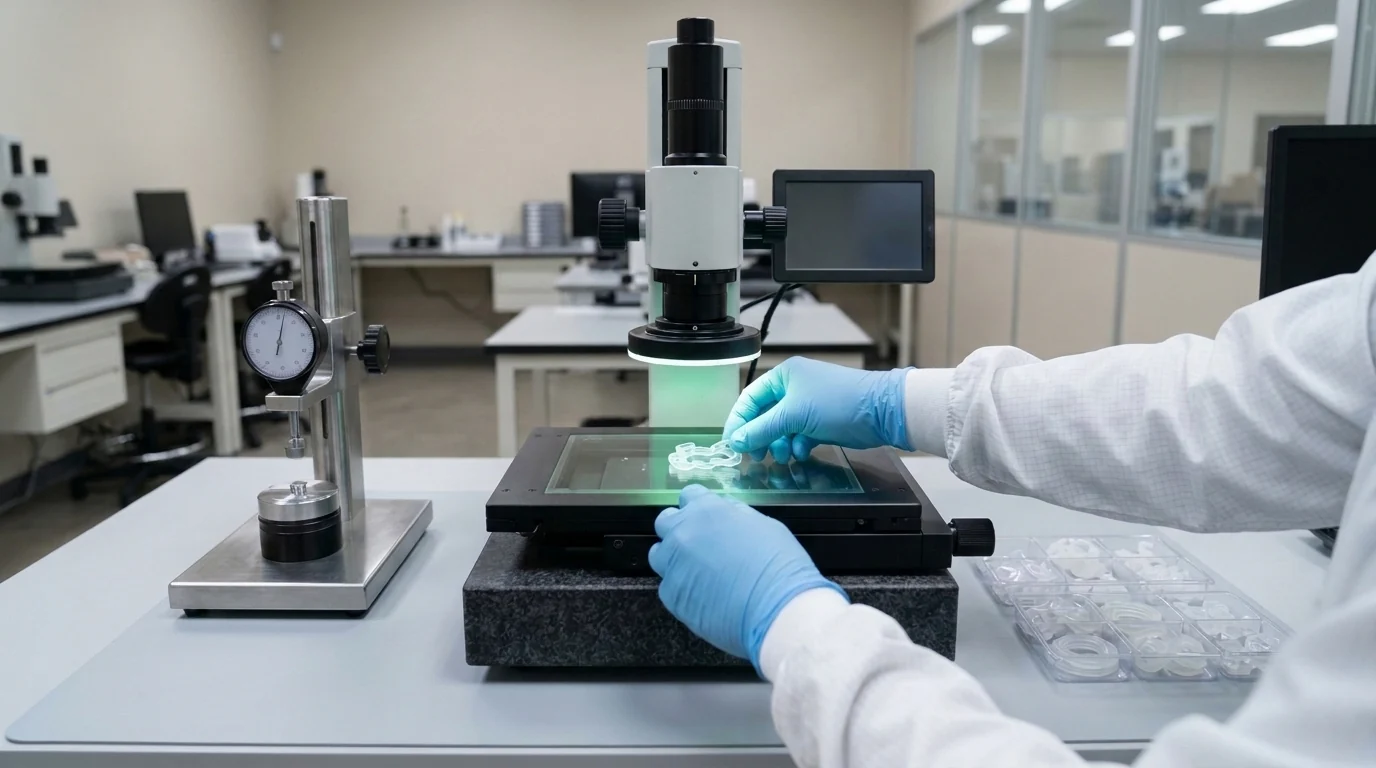
Backlit 2D optical dimensional inspection and Shore A hardness verification bench
Molding Process85T / 120T LSR Overmolding on Customer-Supplied PC Inserts
Material & DurometerSourced Platinum Medical-Grade LSR · 40 Shore A + Customer PC
Key QC Focus±0.05 mm Seal Crown Metrology & Zero Optical-Window Flash
Sampling & Lead TimeT1 in 7–15 days · Mass run 15–30 days

Representative Engineering Program: Illustrates Youbang’s typical mold-shutoff, elastomer compounding and QC workflow for this part geometry. Client-funded molds and proprietary CAD remain strictly protected under NDA.

01 · Engineering Challenge

Eliminating Manual Gasket Twisting, Disinfectant Crevices & Sensor-Window Flash

During pre-production validation of a portable non-implantable monitoring cartridge, manual elastomer ring assembly created three engineering risks:

  • Pinched Rings & Pressure-Decay Leaks: Hand-seating a 1.1 mm seal along a 3D contoured groove caused intermittent twisting and uneven compression.
  • Clinical Wipe-Down Crevices: Daily quaternary ammonium and alcohol disinfection left fluid trapped inside mechanical groove seams and degraded manual cyanoacrylate glues.
  • Tight Lip Height & Keep-Out Zones: Mating latch force required ±0.05 mm seal lip crown repeatability with zero silicone flash encroaching onto adjacent optical windows.
02 · QC & Deliverables

Monolithic Crevice-Free Seal & Full ISO 13485 Bidirectional Traceability

Following the OEM's pressure-decay and disinfectant aging validation on T2 parts, recurring production lots shipped ready for final European cartridge assembly.

  • Flush, peel-verified PC-to-LSR bond interfaces with ±0.05 mm dual-lip crown precision documented via 2D optical metrology and Shore A checks
  • Bidirectional ISO 13485:2016 batch records linking customer-supplied PC insert lots, two-part LSR drum CoAs (with upstream ISO 10993 summaries), and OQC sheets
  • Clean washed and double-PE heat-sealed subassemblies supporting the device manufacturer's own CE/MDR technical file (excluding finished-device licensing)

03 · Tooling & Process Execution

Silane Primer Treatment, Mechanical Shutoff Interlocks & Optical Metrology

We paired controlled chemical adhesion with physical retention features, compensating steel shutoffs, and post-molding clean-zone inspection.

01

3D Frame Verification & Dual Chemical-Mechanical Retention

Supplied free 1–3 pc 3D-printed prototypes (shipping covered by client) once CAD and quote were confirmed to check mating housing clearance, then combined controlled silane primer treatment along silicone-free customer-supplied PC bonding lands with 0.6 mm dovetail grooves and through-hole mechanical interlocks.

02

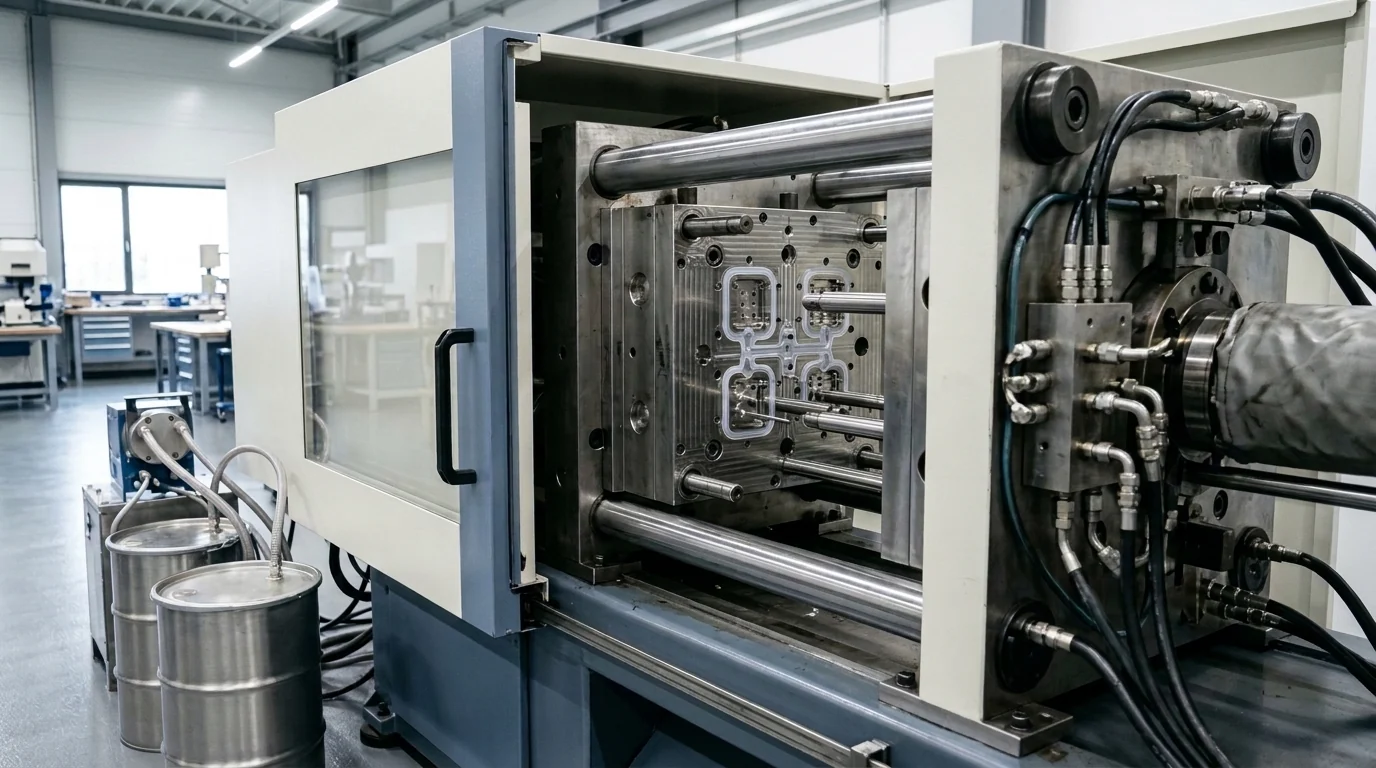
Compensating Shut-Off Lands on 85T/120T LSR Injection Tooling

Designed precision shutoff shoulders around keep-out sensor windows and balanced clamping and curing temperatures comfortably below the customer-supplied PC substrate's heat deflection limit to prevent insert crushing or thin-film flash.

03

2D Optical Vision Metrology & 150–200 m² Clean Zone Packing

Verified 15 critical sealing dimensions on our backlit 2D optical vision measuring system (making a 0.03 mm steel-safe lip crown refinement for T2), followed by washing, visual inspection, and double-PE bag heat-sealing in our 150–200 m² post-molding clean zone.

Silane Primer Treatment, Mechanical Shutoff Interlocks & Optical Metrology
Horizontal LSR injection molding setup with multi-cavity stainless steel mold and A/B metering drums

B2B Factory Direct · 24h Engineering & Tooling Review

Evaluating LSR or HCR Overmolding on Customer-Supplied PC, PP, PA, or Metal?

Share both bare-insert and overmolded assembly 3D CAD files, substrate resin grade/TDS, and keep-out zones. General Manager Zhou Li and our Dongguan engineering team will return a shutoff & bonding DFM review within 24 hours.

✓ NDA available before CAD exchange✓ Eligible for 1–3 free 3D fit prototypes✓ Paid molds 100% owned by customer

Helpful RFQ Inputs

  • 3D STEP + 2D tolerance drawings for both the customer-supplied insert and silicone seal
  • Exact substrate grade (PC, PP, PA, stainless steel, aluminum, or copper) & HDT data
  • Critical sealing tolerances, no-flash keep-out surfaces, and pilot/quarterly lot sizes