
Representative Engineering Program · Kitchen & Barware · Steel-Rim Overmolding + LFGB Post-Cure

Steel-Rim Overmolded Lidded Ice Tray & Mirror Chocolate Mold for LFGB Retail

Manufacturing a stackable lidded square ice cube tray and companion praline chocolate mold for a European kitchenware brand—combining customer-supplied 304 stainless steel frame overmolding, SPI A-1 mirror cavity cores, and full 4-hour 200 °C ventilated post-curing to pass strict German LFGB volatile and sensory panels.

Steel-Rim Overmolded Lidded Ice Tray & Mirror Chocolate Mold for LFGB Retail
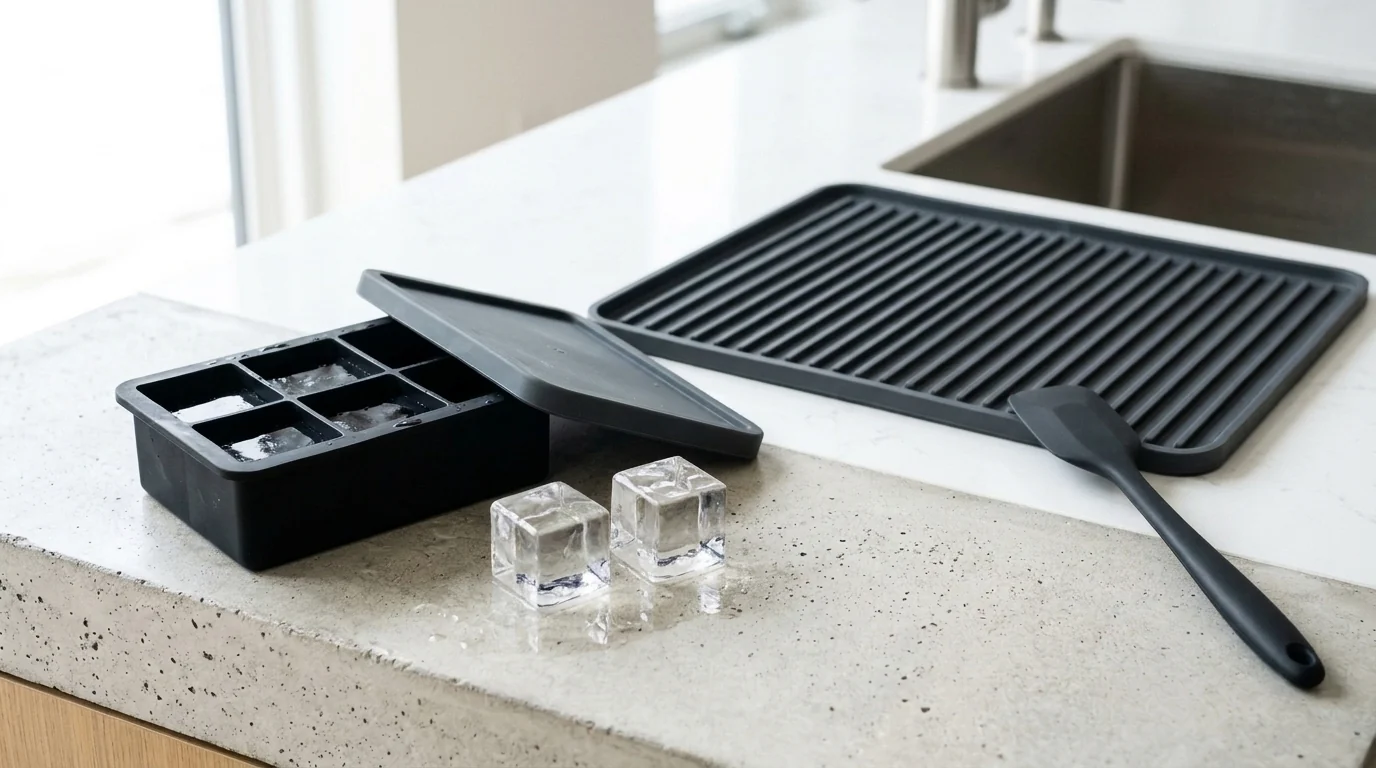
Matte black large-cube silicone ice tray with charcoal lid, graphite ribbed dish-drying sink mat and seamless black silicone spatula
Molding Process200–250T HCR Overmolding on 304 Steel + ~200 °C × 4 h Post-Cure
Material & DurometerPlatinum-Cured Food-Contact Silicone + Customer 304 Stainless Rim
Key QC FocusLFGB Volatile Loss ≤ 0.5% & Zero Organoleptic Odor/Taste Transfer
Sampling & Lead TimeT1 in 7–15 days · Mass run 15–30 days

Representative Engineering Program: Illustrates Youbang’s typical mold-shutoff, elastomer compounding and QC workflow for this part geometry. Client-funded molds and proprietary CAD remain strictly protected under NDA.

01 · Engineering Challenge

Meeting Strict German LFGB Volatile Limits, Spill-Free Carrying & Glossy Release

Supplying European department stores and culinary retailers required solving three stringent compliance and structural demands:

  • German LFGB BfR XV Volatile & Sensory Thresholds: Finished dark-colored silicone had to achieve ≤ 0.5% volatile organic matter loss (200 °C × 4 h) plus zero odor or taste transfer into water and ice.
  • Tray Flexing & Freezer Odor Ingress: Unreinforced silicone trays sagged and spilled water when carried from sink to freezer, while loose lids let freezer odors taint ice over 48 hours.
  • Chalky Chocolate Surface Finish: Standard machined mold cavities left micro-toolmarks that turned tempered dark chocolate matte instead of glossy.
02 · QC & Deliverables

Pass-First-Time LFGB Clearance & Spill-Free Freezer Stacking

After third-party LFGB BfR XV report sign-off, mass production shipped in partner-supplied retail sleeves within standard lead times.

  • Verified ≤ 0.5% volatile organic weight loss and pass grades on LFGB organoleptic odor/taste and overall migration tests via accredited third-party lab
  • Completely encapsulated, flash-free 304 stainless perimeter rims and -20 °C flexible cavity bottoms verified via 2D optical and durometer QC
  • Batch traceability linking upstream Wacker/Shin-Etsu/Elkem class platinum compounds, post-cure temperature charts, and OQC release records

03 · Tooling & Process Execution

Silane-Primer 304 Steel Overmolding, Diamond-Polished Cores & Calibrated Oven Racks

We integrated rigid perimeter overmolding, precision partner core polishing, and uncompromised fresh-air post-curing cycles.

01

3D Lid-Fit Prototyping & Silane-Primer Stainless Rim Overmolding

Supplied free 1–3 pc 3D-printed prototypes (shipping covered by client) after CAD and quote confirmation to verify cube volume and interlocking tongue-and-groove lid fit, then overmolded platinum silicone around a customer-supplied 304 stainless steel perimeter ring treated with silane primer—pairing rigid carrying edges with 1.2 mm push-release cavity bases.

02

SPI A-1 Mirror Core Polishing for Glossy Praline Cavities

Designed the 15-cavity chocolate tool in-house and managed SPI A-1 diamond mirror polishing on the partner-machined steel cores so cured silicone cavities imparted a crisp gloss to tempered chocolate while keeping the outer tray frame non-slip matte.

03

Full 200 °C × 4 h Fresh-Air Post-Cure & Accredited LFGB Testing

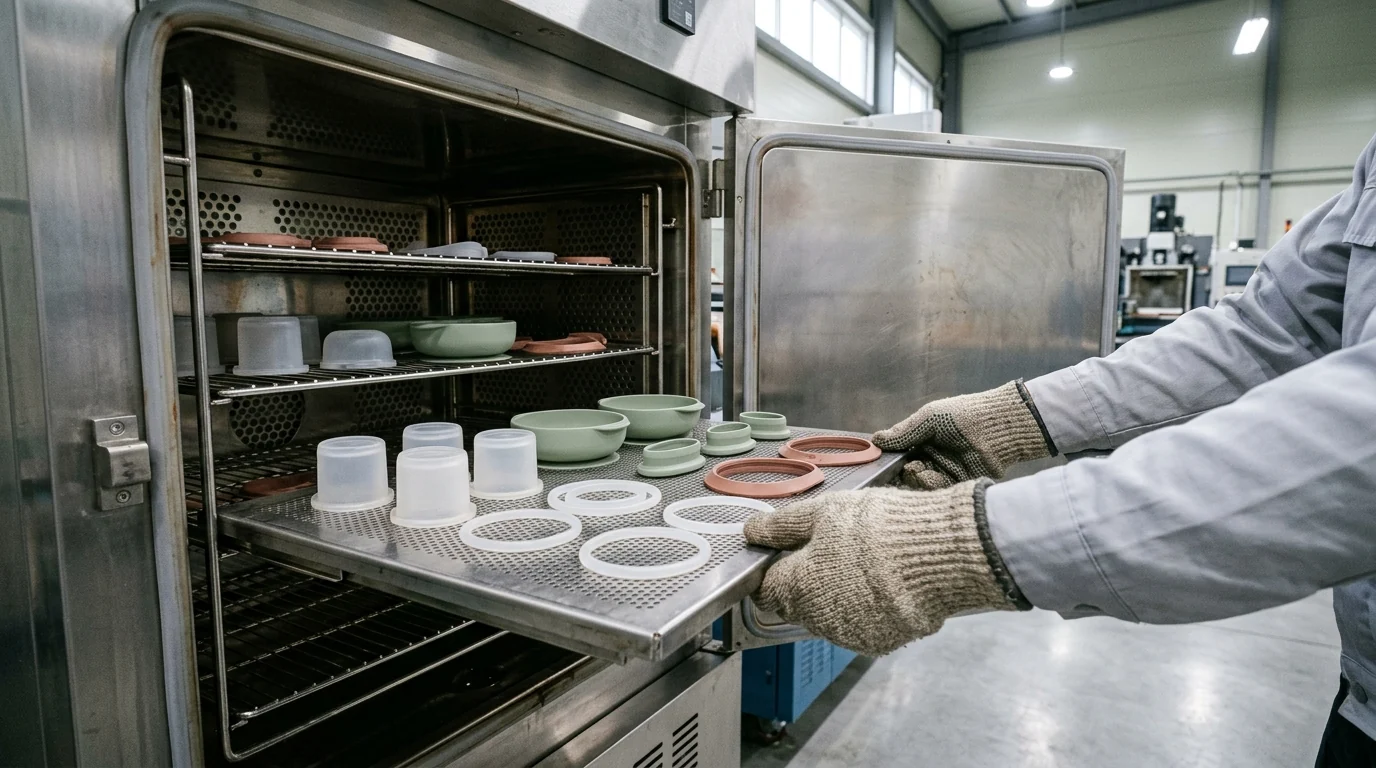
Compounded low-siloxane platinum elastomers with heavy-metal-free inorganic pigments on our mixing mills and enforced a full 4-hour 200 °C ventilated oven post-cure on spaced perforated trays prior to SGS/TÜV LFGB testing (~10 days).

Silane-Primer 304 Steel Overmolding, Diamond-Polished Cores & Calibrated Oven Racks
Perforated stainless steel trays entering a ventilated oven for secondary post-curing (typically 200 °C × 4 h)

B2B Factory Direct · 24h Engineering & Tooling Review

Sourcing LFGB or FDA Compliant Silicone Ice Trays or Confectionery Molds?

Send your 3D CAD files, lid or steel-rim reinforcement concept, and destination testing protocol. General Manager Zhou Li and our Dongguan engineering team will respond within 24 hours with a DFM review and itemized tooling & unit quote.

✓ NDA available before CAD exchange✓ Eligible for 1–3 free 3D fit prototypes✓ Paid molds 100% owned by customer

Helpful RFQ Inputs

  • 3D STEP / IGES drawings for tray, lid, paired sphere mold, or chocolate cavities
  • Customer-supplied 304 stainless / PP / PC insert details (if reinforced or lidded)
  • Target food-contact test standard (LFGB / FDA / Japan MHLW 370) and order quantity